 Skip to content

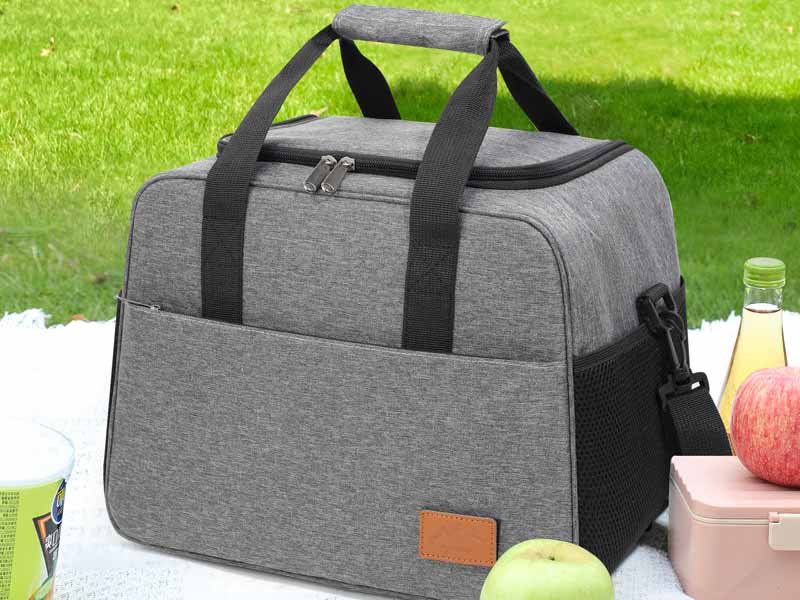
A cooler bag often looks simple in a product photo: an outer shell, a zipper, two handles, some insulation, and a logo. In real product development, however, those visible parts are only the surface. Capacity changes when thicker foam is added. A wide opening makes loading easier but can increase heat exchange. A strong-looking handle may still fail when the bag is filled with bottles, food, and ice packs. Even the liner that looks smooth in an empty sample may wrinkle, stretch, or leak once the product is loaded and used repeatedly.
Designing a custom cooler bag starts with the use case, contents, usable capacity, loaded weight, thermal target, carrying method, cleaning needs, and target market. From there, select the bag format, outer fabric, insulation, liner, closure, reinforcement, branding, and packaging. Build a realistic sample, test it under loaded conditions, correct weak points, and lock the approved specification before bulk production.
The most successful cooler projects usually begin with a surprisingly ordinary question: what will a real person put inside this bag on a normal day? Once that answer is clear, decisions about dimensions, foam, lining, zippers, straps, and cost become much easier. When that answer is vague, the project often spends more time correcting samples than developing the product.
What Should You Define Before Designing a Custom Cooler Bag?

Before choosing fabric, foam, lining, or hardware, define the cooler bag’s real use case, contents, capacity, loaded weight, expected temperature-control period, carrying method, cleaning requirements, sales channel, brand position, packaging needs, and order scale. These points form the product brief and determine which materials and structures are appropriate before sampling begins.
Define the Real Use Case
“Cooler bag” is a product category, not a complete specification. A compact office lunch bag, a 24-can picnic cooler, an insulated grocery tote, a cooler backpack, and a restaurant delivery bag may all use foam and a thermal lining, but they solve very different problems. The first development task is therefore to describe the complete use scenario rather than to choose a shape from a catalog.
Start with the contents. A lunch cooler may hold a rectangular meal container, fruit, a drink bottle, and one or two slim cold packs. A beverage cooler may carry cans, bottles, loose ice, and accessories. A delivery bag may need to accept fixed-size food cartons without tilting or crushing them. These differences immediately influence internal dimensions, opening size, liner construction, wall thickness, pocket layout, reinforcement, and how the bag should be carried.
Loaded weight deserves the same attention. Water and many drinks weigh close to one kilogram per liter, which means a medium cooler can become heavy very quickly. A bag that feels light and comfortable when empty may be carrying more than 10 kilograms once it is filled with beverages, food, cold packs, and ice. That load moves through the handles, shoulder strap, webbing, stitches, side panels, and bottom structure every time the product is lifted.
Environment changes the design as well. A bag carried from home to an office for thirty minutes does not face the same thermal and abrasion conditions as a cooler sitting in a warm vehicle, on a beach, or beside a campsite for several hours. A grocery cooler that is opened once after shopping also behaves differently from a picnic cooler opened repeatedly throughout the day.
A useful early brief should answer:
- What products will usually be carried?
- What are the largest item dimensions?
- What is the likely loaded weight?
- How often will the cooler be opened?
- Will users add loose ice or cold packs?
- Will the bag be carried by hand, shoulder, or back?
- Will it be used mainly indoors, outdoors, or for delivery?
- How often will the liner need cleaning?
- Is compact storage important when the bag is empty?
- What sales channel will the product enter?
These questions give the development team a much stronger foundation than general instructions such as “make it durable” or “make it premium.”
Set Capacity and Performance Targets
Capacity should be described in a way that matches how customers actually use the product. Liters are helpful for comparing overall volume, but a commercial development brief should usually include a second reference such as container dimensions, bottle height, delivery-box size, or a practical can-count format. A 20-liter cooler that is tall and narrow may not accept the same contents as a 20-liter rectangular cooler with a wide lid.
Usable internal volume matters more than external volume. Foam, lining, seam allowances, binding, reinforcement panels, zipper construction, and rounded corners all consume space. A bag with generous external dimensions can therefore feel surprisingly small inside once a substantial insulation system is installed. This effect becomes especially noticeable in compact lunch bags where a few millimeters on each wall can determine whether a meal box fits comfortably.
Thermal expectations also need context. A cooler bag does not actively refrigerate its contents; it slows heat transfer. Its real performance depends on foam type, foam thickness, liner construction, closure design, opening frequency, starting product temperature, amount of cold media, ambient temperature, sunlight, and the amount of empty air remaining inside the bag.
For that reason, performance should be described as a testable use target rather than an unsupported number of hours. A requirement such as maintaining chilled drinks during a typical half-day outdoor outing with a defined quantity of cold packs can be tested consistently. A statement such as “10 mm foam keeps items cold for 12 hours” is much less useful unless the loading method, starting temperature, ambient temperature, and test procedure are also defined.
Build a Practical Product Brief
A good product brief does not need to be fifty pages long. It needs to make important assumptions visible before the first sample is made. The document should capture both physical requirements and commercial constraints so the development team understands not only what the cooler should look like, but also where it will be sold and what the final product must achieve.
A practical custom cooler bag brief normally includes:
- Target user and primary use
- Approximate external dimensions
- Minimum usable internal dimensions
- Desired liter or can capacity
- Typical loaded weight
- Preferred bag format
- Outer material direction
- Insulation expectation
- Lining preference
- Closure type
- Handle and shoulder-strap requirements
- Pocket layout
- Logo method
- Brand colors
- Label requirements
- Retail or e-commerce packaging
- Target quantity
- Target market
- Intended retail position
When a reference sample already exists, identify what should be retained and what should be improved. A competitor product may have the correct capacity but weak handles, good insulation but difficult cleaning, or attractive styling but a narrow opening. A development team can learn much more from those observations than from a request to “make the same product with our logo.”
Balance Performance, Weight, and Cost
Every cooler bag specification involves trade-offs. Thicker insulation can improve resistance to heat transfer, but it also reduces usable space, increases weight, raises material consumption, and can make the product harder to sew. A heavy-duty fabric may resist abrasion better but create more shipping weight. A high-specification zipper may improve durability and closure performance while increasing cost and opening resistance.
A useful approach is to decide whether the product is primarily value-focused, mainstream branded, performance-oriented, premium outdoor, delivery-focused, or promotional. A value-focused lunch cooler may work well with standard polyester or Oxford fabric, moderate foam, a practical PEVA or aluminum-film liner, standard webbing, and straightforward printing. A performance-focused outdoor cooler may justify a tougher shell, thicker insulation, a reinforced base, stronger webbing, upgraded closures, and more structured side walls.
The goal is not to select the most expensive component in every category. A strong specification is one in which the material, insulation, liner, structure, branding, and price support the same market position. Products usually become difficult to manufacture or sell when one part of the specification is far more ambitious than the rest.
Which Cooler Bag Type, Size, and Capacity Should You Choose?

Choose the cooler format according to what will be carried, how the bag will be opened, how far it will be carried, how much structure is needed, and where it will be sold. Calculate capacity from usable internal dimensions rather than outside dimensions alone because insulation, seams, curved corners, panels, and reinforcement can noticeably reduce interior space.
Choose the Right Cooler Format
Soft coolers are versatile because they can be built in many sizes, compressed for storage, and adapted to outdoor, beverage, retail, or lifestyle uses. Cooler backpacks are more suitable when users walk longer distances and need their hands free. Insulated totes favor quick access and grocery-style loading, while lunch coolers usually prioritize compact size and convenient organization. Delivery coolers often need a rectangular body, wide opening, stronger bottom support, and reinforced carrying points.
| Cooler Bag Type | Typical Capacity Range | Main Priority | Common Design Challenge |
|---|---|---|---|
| Lunch cooler | 4–10 L | Compact daily use | Container fit and cleaning |
| Small soft cooler | 8–18 L | Portable outdoor use | Capacity vs. wall thickness |
| Medium soft cooler | 18–30 L | Picnic and beverage use | Loaded weight and handles |
| Cooler backpack | 15–30 L | Hands-free carrying | Strap comfort and balance |
| Insulated tote | 15–35 L | Grocery and lifestyle use | Wide access and shape control |
| Delivery cooler | 25–80+ L | Food transport | Box fit, structure, and load |
These figures are useful development references rather than fixed standards. Two products with the same liter capacity can behave very differently if one is tall and narrow while the other is wide and rectangular. Before choosing a style, place representative contents on a table and look at how they naturally want to be arranged. The best bag shape often becomes obvious when the physical load is considered first.
Calculate Usable Capacity
For a basic rectangular compartment, theoretical volume can be estimated by multiplying internal length, width, and height. An interior measuring 36 × 22 × 24 centimeters has a theoretical rectangular volume of about 19 liters. Actual usable capacity will normally be lower because corners, liner folds, seams, zipper paths, partitions, and structural materials occupy part of that space.
This is an important distinction because external dimensions can be misleading. Imagine a cooler with outside dimensions of 40 × 28 × 30 centimeters. A simple external-volume calculation suggests more than 30 liters, but that number does not represent usable capacity. Once an insulated wall system is added to each side, along with a thicker base, lid, lining, zipper, and seam construction, the internal volume can decrease substantially.
Capacity should therefore be checked in three ways. First, calculate theoretical internal volume. Second, load the sample with real or representative contents. Third, check whether those contents can be inserted and removed comfortably. A design that technically fits twelve cans may still feel poorly designed if users must force the final cans past a narrow zipper opening.
For lunch bags and delivery products, actual container dimensions are often more useful than nominal liter capacity. If the product is built around a specific food box or bottle, design around that object and provide reasonable clearance rather than relying only on a volume calculation.
Allow for Insulation Thickness
Insulation takes space from opposing walls. If the total insulated wall construction increases by 5 millimeters on both sides, the interior loses approximately 10 millimeters of width. The same effect occurs along the length and height where insulation is present. In compact cooler bags, those reductions can determine whether the intended container fits correctly.
Consider an external lunch-bag width of 220 millimeters. If the combined wall build from shell, foam, lining, and construction becomes about 15 millimeters on each side, the remaining theoretical internal width is already close to 190 millimeters before seam allowances and corner shape are considered. A food box measuring 185 millimeters wide may fit on paper but leave too little clearance for comfortable daily use.
Thicker insulation also influences zipper installation, corner radius, side-wall stiffness, folding behavior, packing volume, and sewing difficulty. This is one reason size and insulation should be developed together. Selecting the exterior dimensions first and adding a thicker foam system later often creates unexpected capacity problems.
When an external size is fixed because of shelving, packaging, lockers, vehicle compartments, or delivery racks, the development team must decide whether usable capacity or insulation thickness is more important. Making that decision before sampling saves considerably more time than trying to recover lost capacity after the basic pattern is approved.
Design Around Loaded Weight
Capacity also determines structural load. A medium cooler filled with beverages can become much heavier than its empty appearance suggests. Twelve liters of drinks alone can approach 12 kilograms, before the weight of the bag, containers, food, and cold packs is added. Larger picnic or delivery coolers can carry substantially more.
That weight must travel through every part of the carrying system. Webbing width, stitch pattern, side-panel reinforcement, D-rings, buckles, base structure, and shoulder padding should therefore be selected according to real loaded conditions. Medium and larger coolers commonly benefit from wider webbing in the 38–50 millimeter range where comfort and load distribution are priorities, although the correct width still depends on the particular product.
Longer webbing attachment zones can spread load across a larger area of the side panel, while reinforced stitch patterns can reduce stress concentration at handle ends. Shoulder straps need enough width and padding to remain comfortable when the product is loaded rather than only when it is displayed empty.
A good capacity is therefore not simply the largest number of liters that can fit within a target footprint. It is the amount users can load, close, lift, carry, set down, and reopen without overstressing the product or making it unpleasant to handle.
Which Materials and Insulation Are Best for a Cooler Bag?

There is no single best cooler bag material. The right construction combines the outer shell, insulation, inner liner, zipper, reinforcement, and carrying components for a specific use case. Polyester and Oxford work well for many mainstream products, while tarpaulin and TPU-based materials can suit tougher applications. PEVA, aluminum-film, TPU, and PVC liners each involve different cost and manufacturing considerations.
Choose the Outer Shell
The outer material determines much of the bag’s abrasion resistance, appearance, hand feel, print compatibility, weight, and perceived quality. It also affects how the product behaves after repeated folding, cleaning, and exposure to outdoor conditions. A basic promotional lunch cooler therefore does not need the same shell as a soft cooler designed for frequent camping and rough vehicle use.
Polyester and Oxford fabrics are widely used because they offer a practical balance of cost, availability, durability, color choice, and decoration compatibility. Depending on the product, common specifications may start around 300D for lighter designs and move to 600D, 900D, 1200D, or heavier constructions when greater structure and abrasion resistance are required.
A 600D polyester or Oxford construction is often a sensible starting point for mainstream retail coolers, but the denier number alone does not describe the final material. Coating, yarn construction, backing, finished weight, weave, and surface treatment can create meaningful differences between two fabrics both sold under the same general description.
Tarpaulin and TPU-laminated materials are more common in performance-oriented or premium outdoor products. Their smoother surfaces can be easier to wipe and can create a more technical appearance. They may also support different seam or welding techniques. However, stiffness, lamination quality, cold-temperature flexibility, print compatibility, and production method need to be reviewed during development.
Match the Insulation to the Product
Foam is central to a cooler bag, but thickness alone does not define performance. Different foam types vary in density, flexibility, compression resistance, recovery, structure, cost, and how well they maintain continuity around corners and seams.
| Layer | Common Options | Typical Design Consideration |
|---|---|---|
| Outer shell | 300D–1200D+ polyester/Oxford | Abrasion, weight, printing, cost |
| Technical shell | Tarpaulin, TPU-laminated fabric | Outdoor use, cleaning, structure |
| Insulation | PE, EPE, XPE, EVA, PU foam | Thickness, density, recovery |
| Inner liner | PEVA, aluminum film, TPU, PVC | Cleaning, seams, flexibility |
| Reinforcement | PE/PP board, EVA, stiff panels | Shape and load support |
| Carry system | Polyester or nylon webbing | Width, strength, comfort |
PE and EPE foams are widely used in mainstream insulated bags because they are lightweight and practical for sewn construction. XPE can provide a more consistent closed-cell structure depending on specification. EVA is useful where greater resilience or structure is required. PU foam can be considered in certain higher-insulation constructions, although the manufacturing method may differ from a simple sheet-foam cooler.
In lightweight promotional or lunch coolers, foam thicknesses around 3–5 millimeters are common starting references. More substantial soft coolers may use approximately 8–15 millimeters, while performance-oriented products may use thicker or multi-layer systems. These numbers are specification ranges, not promises of a fixed number of cold-retention hours.
During sample review, check not only nominal thickness but also how much the foam is compressed by binding, stitching, and structural seams. A nominal 10-millimeter panel may perform differently if large portions are compressed aggressively around the perimeter.
Select the Inner Lining
The inner liner faces condensation, spills, grease, food residue, cleaning, folding, and repeated stress. Its performance therefore needs to be evaluated from both a material and construction perspective.
PEVA is widely used in mainstream lunch and cooler bags because it is flexible and relatively easy to wipe clean. Aluminum-film liners are common in cost-sensitive or general-purpose insulated bags and can work well when combined with an appropriate foam system. TPU can suit more demanding or premium constructions, especially when flexible welded liner systems or improved durability are required. PVC also appears in some insulated products, although target-market material requirements should be reviewed before final selection.
A liner evaluation should consider:
- Thickness
- Flexibility
- Tear behavior
- Ease of cleaning
- Odor
- Corner stress
- Seam method
- Compatibility with welding or stitching
- Performance when folded
- Market-specific material requirements
The material name alone cannot guarantee leak control. A strong liner can still fail if corners are poorly designed or seam transitions create weak points. When the product will contain loose ice or substantial condensation, liner construction becomes one of the most important engineering areas in the entire bag.
Understand the Complete Thermal System
Cold retention depends on the entire thermal envelope. Foam slows heat movement through the side walls, but the lid, zipper, corner joints, seams, and frequent opening can create faster paths for heat exchange. Increasing foam thickness everywhere may provide limited benefit if the main weakness is actually the closure or lid design.
Loading conditions matter just as much. A tightly packed bag containing pre-chilled beverages and several cold packs generally behaves differently from a half-empty bag containing warm items. Empty air volume, starting temperature, cold-pack quantity, and opening frequency all influence the temperature curve.
Ambient conditions can change results significantly as well. A cooler tested indoors at approximately 20°C cannot be compared directly with the same product sitting in direct sun at 35°C. Dark outer fabrics can also absorb more solar heat under certain conditions than light-colored surfaces.
When comparing prototypes, control the variables:
- Use the same contents.
- Use the same starting temperature.
- Use the same amount of cold media.
- Maintain similar ambient conditions.
- Position temperature sensors consistently.
- Use the same opening schedule.
- Record readings at fixed intervals.
This type of comparison can show whether a thicker foam system, improved lid, or better closure actually creates measurable improvement. It also provides a stronger basis for product claims than relying on a supplier’s generic statement about insulation hours.
How Should You Design the Cooler Bag Structure?

A cooler bag structure should keep insulation reasonably continuous, reduce unnecessary heat exchange, contain condensation or spills, remain easy to clean, carry the expected load, and preserve the intended shape. Pay particular attention to the lid, zipper path, liner corners, bottom, handle attachments, shoulder straps, and reinforcement zones because many real failures occur where different components meet.
Control the Opening and Closure
The opening is one of the clearest examples of competing design priorities. A large U-shaped lid makes it easy to see, load, and remove contents, which is useful for lunch bags, picnic coolers, and delivery products. At the same time, a large opening allows more air exchange whenever the bag is opened. Smaller openings can reduce exposure but may make the product frustrating to use.
The correct balance depends on how often customers need access. A delivery cooler may be opened many times in a short period, making speed and box clearance more important. A soft cooler used for a day outdoors may benefit from a more controlled opening if users do not need to expose the entire compartment every time they reach for a drink.
Zipper choice also changes the experience. Standard coil zippers are practical and cost-efficient for many mainstream products. Larger-gauge zippers can offer greater durability where the bag is opened frequently. Water-resistant zipper options can help with certain performance goals, but they normally cost more, feel stiffer, and may require greater pulling force.
The zipper path deserves careful sampling. Tight-radius corners can create excessive resistance, especially when thick foam is compressed around the lid. The sample should therefore be opened and closed repeatedly when both empty and fully loaded. A zipper that feels smooth on an empty development sample can become noticeably harder to operate when the cooler walls deform under load.
Design for Leak Resistance and Cleaning
Water resistance on the outside does not automatically make a cooler leak-proof. Liquid can escape through liner seams, stitched corners, zipper openings, drainage areas, and transitions between different materials. The level of leak control should therefore be defined according to the real use case.
A typical lunch cooler may only need to contain condensation and minor food spills. A soft cooler intended to hold loose ice may require a more controlled liner, seam, and corner system. Those products should not use identical performance language because the construction requirements are different.
Useful design measures can include smoother liner corners, treated or welded seams where appropriate, raised seam locations, more controlled transitions around the lid, and a base designed to avoid unnecessary stress points. Cleaning should be considered at the same time. A liner may be technically wipeable but still unpleasant to maintain if deep folds trap crumbs, sauces, or moisture.
Prototype evaluation should include a defined leakage procedure rather than an informal check. Record the amount of liquid used, how long it remains inside, whether the bag is moved or tilted, and where the product is inspected afterward. Repeatable tests make design changes easier to compare and reduce disagreement between development and QC teams.
Engineer the Carrying System
Cooler bags experience most of their structural stress after loading. Handles, straps, D-rings, buckles, stitching, side panels, and the bottom structure must work together rather than being treated as separate accessories.
For medium and large coolers, webbing often needs to extend farther down the side wall so the load is spread over a larger area. Reinforcement pieces can help prevent the handle attachment from concentrating force into one small section of fabric. Box-and-cross or comparable reinforced stitch patterns are commonly used at high-stress webbing locations, although the exact method should match the material and production process.
Shoulder comfort is another practical issue. A strap that is acceptable at two kilograms may become uncomfortable at ten kilograms. Width, padding, adjustment range, hardware position, and attachment angle all influence how the load feels during real use. A cooler backpack requires even more attention because shoulder-strap geometry, back-panel padding, and center of gravity affect the entire carrying experience.
Testing should reflect the intended payload. A handle strength check for a small lunch bag should not use the same assumptions as a test for a 30-liter beverage cooler. The relevant question is whether the complete carrying system remains secure and comfortable under the load the product is genuinely expected to carry.
Keep the Shape Stable
Not every cooler should stand perfectly upright. Some products are intentionally soft and collapsible because compact storage is part of their value. Others, particularly delivery coolers, premium outdoor coolers, and retail products, need enough structure to maintain their shape during loading and use.
Shape can be controlled through foam density, thicker panels, PE or PP board, EVA reinforcement, structured bottom inserts, piping, binding, or molded EVA sections. A rigid or semi-rigid base can help bottles remain upright and reduce sagging. Side-wall reinforcement can make a large delivery cooler easier to load because the opening does not collapse inward.
More structure is not always better. Reinforcement increases weight, material usage, packing volume, and often shipping cost. A bag that can no longer fold may occupy several times more carton volume than a softer alternative. That difference can become important for e-commerce programs or large international shipments.
The right structure should be evaluated with representative contents. An empty cooler can look excellent during photography but still collapse once it is filled with heavy bottles. Load testing reveals where reinforcement is actually needed and prevents unnecessary stiffness in areas that do not contribute much to performance.
How Do You Add Custom Branding to a Cooler Bag?
Branding should be developed alongside the material and structure, not added after the product is finished. Logo method, placement, webbing, zipper pullers, labels, colors, and packaging should work as one visual system. Screen printing, heat transfer, embroidery, woven labels, rubber patches, and silicone patches each suit different materials, artwork styles, durability expectations, and price positions.
Match the Logo Method to the Material
A logo that looks sharp on smooth polyester may behave very differently on textured Oxford, tarpaulin, or coated TPU fabric. Branding method should therefore be selected after the main material direction is known.
Screen printing is practical for many solid-color logos and larger production runs. It can be cost-effective and visually strong when the fabric surface and ink system are compatible. Heat transfer is useful for detailed graphics, smaller text, and artwork with more color variation, although transfer film, adhesive, temperature, pressure, and coating compatibility should be checked on the actual production material.
Embroidery creates a textile-rich appearance and works particularly well for lifestyle or premium fabric bags, but it also adds needle penetration and local stiffness. Dense embroidery can distort thin panels or conflict with highly coated materials. Woven labels create a subtle, clean identity and can be applied across several SKUs with consistent proportions. Rubber and silicone patches are common on outdoor products because they provide a dimensional appearance and can hold detailed molded artwork.
Every logo sample should be checked for:
- Final dimensions
- Edge definition
- Color match
- Adhesion or stitch quality
- Surface distortion
- Flexing
- Abrasion exposure
- Position after loading
A digital rendering is useful for checking scale and layout, but final approval should always be based on the real logo applied to the real material.
Place the Logo Where Customers See It
The biggest blank panel is not always the best branding area. Pockets, side seams, handles, straps, and the normal carrying orientation all influence visibility. A logo can look perfectly centered on a flat pattern and appear awkward after the bag is filled.
A cooler backpack usually presents the front panel to the viewer, while an insulated tote may present either large side panel. A shoulder-carried soft cooler often exposes one panel more than the other. Delivery products may need identification from several directions because they are viewed while stacked, carried, or loaded into vehicles.
Logo scale should suit the product position. Promotional coolers may intentionally use a large 150–250 millimeter graphic because visibility is central to the project. Premium outdoor products often use smaller patches or woven branding in the 40–80 millimeter range for a more understated appearance. These are design references rather than strict rules.
Avoid placing key branding across tightly curved areas, major seams, high-abrasion zones, or surfaces that are constantly compressed during packing. If the product will become part of a larger collection, establish a consistent placement system so lunch bags, totes, backpacks, and soft coolers feel connected even when their shapes are different.
Build a Complete Brand System
Private labeling is more than placing one logo on the front of a generic bag. Main fabric, secondary panels, webbing, zipper tape, pullers, buckles, binding, labels, hangtags, interior marks, retail packaging, and shipping cartons all contribute to the finished brand experience.
A coordinated cooler bag can include:
- Main shell color
- Accent-panel color
- Custom webbing
- Coordinated zipper tape
- Custom zipper puller
- Woven label
- Care label
- Rubber or silicone patch
- Printed interior element
- Hangtag
- Barcode label
- Retail packaging
- Shipping carton marks
Color control deserves realistic expectations because different substrates reflect light and accept pigments differently. A gray polyester fabric, gray nylon webbing, gray plastic buckle, and gray printed logo may never appear perfectly identical even when each is close to the same Pantone target. The objective is controlled visual harmony, not an unrealistic promise that every material will reproduce color in exactly the same way.
For multi-SKU collections, approved swatches and component samples help maintain consistency. If a brand uses the same navy shell, black webbing, molded puller, and rubber patch across several products, retaining those references makes future development and repeat orders much easier.
For complex programs, it can be useful to review the fabric, insulation, webbing, logo, packaging, and production implications together during sampling. Lovrix can support this type of product-development discussion when a project requires multiple materials or coordinated brand details, but the final choices should still be driven by the product’s real use case and market position.
Plan for Repeat Orders
A good first order should be capable of becoming a good fifth order. That requires more than saving an old photograph. Fabric, coating, webbing, zipper, foam, liner, logo, and packaging details need enough documentation for the product to be reproduced consistently.
Brand-critical specifications commonly include:
- Fabric construction
- Approved color reference
- Coating or backing requirement
- Webbing width and thickness
- Zipper size and shade
- Puller finish
- Logo dimensions
- Logo location
- Label artwork version
- Packaging version
Small uncontrolled substitutions can gradually change a product. A slightly different gray webbing, thinner foam, another zipper gauge, or a different rubber-patch finish may appear minor individually but become noticeable across a collection.
Repeatability becomes especially important when a successful cooler expands into multiple colors and sizes. Shared components can simplify production and purchasing, but only when approved specifications are maintained. Development documentation is therefore not administrative paperwork; it protects the visual and functional identity of the product after the original team moves on to other projects.
How Do You Sample, Test, and Prepare for Bulk Production?
Sampling should prove that the cooler works under realistic conditions, not simply that one attractive prototype can be sewn. Check dimensions, usable capacity, insulation, liner construction, leak resistance, zipper operation, carrying comfort, structure, branding, cleaning, and packaging. Once approved, convert the sample into controlled specifications so production and QC teams can reproduce the same product consistently.
Test the Sample Like a Real User
The first prototype should be treated as a working product rather than a display sample. Start with dimensions and appearance, but move quickly into actual use. Place the intended food boxes, cans, bottles, or delivery containers inside. Add the planned cold packs. Close the product, carry it, place it on the ground, reopen it, use the pockets, and remove the largest item.
This process often reveals problems that a drawing cannot show. The opening may be one centimeter too narrow. The shoulder strap may force a large cooler to tilt. A bottle pocket may interfere with the main zipper. The lid may compress tall contents. The liner may pull tightly at one corner when the bag is loaded.
A practical sample review can record:
- External dimensions
- Internal usable dimensions
- Capacity
- Empty weight
- Loaded weight
- Foam thickness
- Wall stiffness
- Liner condition
- Zipper operation
- Handle comfort
- Shoulder-strap comfort
- Pocket access
- Logo position
- Packing dimensions
Comments should be specific. “Make it more premium” does not give the sample room enough direction. “Increase the base reinforcement so the bottom remains flatter under a 10-kilogram load” is measurable and can be checked on the next revision.
Use Tests That Match the Product
Different cooler bags have different risks. A lightweight promotional lunch bag does not need exactly the same testing plan as a premium outdoor soft cooler, a 50-liter delivery bag, or a temperature-sensitive transport product. Tests should focus on the failures that matter most for the intended application.
| Test or Check | Practical Purpose | Useful Measurement |
|---|---|---|
| Dimension check | Confirm product size | mm against approved tolerance |
| Capacity check | Verify usable interior | liters or real load configuration |
| Foam check | Confirm insulation build | thickness in mm |
| Leakage check | Identify liner weak points | defined water volume and time |
| Handle load check | Check carrying strength | defined kg load and duration |
| Strap pull check | Check attachment security | defined force or load |
| Zipper cycling | Evaluate repeated operation | agreed open-close cycles |
| Thermal comparison | Compare insulation versions | temperature over time |
| Logo adhesion | Check decoration durability | agreed rub or peel method |
| Packing check | Confirm shipping suitability | carton count and condition |
Thermal comparisons require especially careful control. If Prototype A is tested with six frozen packs and Prototype B with two chilled packs, the results cannot meaningfully show which structure is better. Use the same contents, starting temperature, ambient environment, cold-pack quantity, probe position, opening schedule, and test duration.
The same logic applies to load tests and leakage tests. A number without a defined procedure can sound precise while providing very little useful evidence. A repeatable method makes it possible to compare revisions and creates a stronger basis for quality specifications later.
Lock the Production Specification
Once the final sample is approved, the project needs to move from a physical prototype to a production standard. The approved sample remains important, but it should be supported by documents that describe the components and critical details clearly enough for the bulk-production team to repeat them.
The production package normally includes:
- Approved physical sample
- Pattern version
- Bill of materials
- Main fabric specification
- Lining specification
- Foam type and thickness
- Reinforcement materials
- Webbing specification
- Zipper specification
- Buckles and hardware
- Logo artwork and size
- Logo placement
- Product dimensions
- Color standards
- Labels
- Packaging
- Carton marks
- Agreed inspection points
For conventional sewn cooler projects, a development sample may commonly require approximately 5–15 working days depending on materials, structure, insulation, logo process, and packaging. Simple revisions may be faster, while molded EVA, special fabrics, customized webbing, complex printing, or unusual packaging can require additional time.
Bulk production planning also depends on material availability, order quantity, SKU count, testing, packaging, and factory scheduling. Straightforward projects may often be planned around roughly 25–35 days after final sample and material approval, while more complex structures, multi-SKU programs, or special-material projects may move closer to 35–60 days. These figures are planning references rather than automatic guarantees and should be confirmed against the final product specification.
Prepare for Consistent Bulk Production
Quality control begins before the sewing line. Incoming materials should be checked against approved references so differences in fabric color, coating, foam thickness, liner quality, webbing, zipper, or branding are identified before they become thousands of finished products.
Typical incoming checks may include fabric shade, coating condition, foam thickness, liner appearance, zipper operation, webbing width, hardware finish, and logo quality. During production, dimensional control, seam construction, foam placement, handle reinforcement, liner assembly, zipper installation, and logo position become important checkpoints.
Final inspection can review product appearance, dimensions, opening and closing, carrying points, liner condition, packaging, labels, carton quantity, and any functional tests agreed during development. The exact inspection plan should reflect the product’s real risks rather than becoming an unnecessarily long checklist copied from an unrelated bag.
Repeat orders make documentation even more valuable. Approved patterns, BOM versions, material references, color swatches, packaging files, and final samples can reduce inconsistency when the product is produced again months later. The strongest test of a production-ready design is simple: another production team should be able to recreate the product from the approved records without relying on one person’s memory.
Conclusion
Designing a custom cooler bag is not a matter of choosing a shell fabric, adding foam, and printing a logo. The decisions are connected. Increasing insulation can reduce capacity. Enlarging the opening can improve loading but change thermal behavior. Stronger materials can improve durability while increasing weight and cost. A larger bag creates new load requirements for handles, shoulder straps, seams, and the base.
The most reliable development process begins with use, contents, capacity, and loaded weight. It then moves through material selection, insulation, lining, structure, branding, sample validation, and production control. Each stage should answer a practical question about how the finished cooler will behave in the hands of a real customer.
A well-developed cooler bag does not need the thickest foam, the most expensive zipper, or the longest feature list. It needs the right combination of specifications for its intended market. When the final sample can be loaded naturally, carried comfortably, cleaned easily, tested consistently, branded correctly, and reproduced from clear production records, the design has moved beyond looking good. It has become a product that can support real commercial use and reliable repeat production.
Frequently Asked Questions
What is the best material for a custom cooler bag?
There is no single best material for every cooler bag. Polyester and Oxford fabrics are practical for many lunch, retail, promotional, and mainstream soft coolers because they balance cost, durability, and branding flexibility. Tarpaulin and TPU-laminated fabrics are more common when greater abrasion resistance, wipe-clean performance, or a technical outdoor appearance is required. The outer material should be selected together with insulation, lining, zipper construction, expected load, and target price rather than in isolation.
How thick should cooler bag insulation be?
Insulation thickness depends on the size, use case, target performance, and internal-capacity requirement. Lightweight lunch or promotional coolers may use foam around 3–5 millimeters, while more substantial soft coolers commonly move into approximately 8–15 millimeters or more. Thickness alone does not determine cold retention, because foam type, density, lid design, zipper, liner, opening frequency, loading conditions, and ambient temperature all influence performance. Prototype testing under repeatable conditions is more reliable than selecting foam based only on a thickness number.
Is PEVA or aluminum foil better for cooler bag lining?
PEVA and aluminum-film liners serve different product positions rather than forming a simple better-or-worse comparison. PEVA is flexible, easy to wipe, and widely used in mainstream insulated bags. Aluminum-film liners are common in general-purpose and cost-conscious products and can work effectively with appropriate foam. TPU may be considered for more demanding constructions. Liner selection should also consider thickness, seam method, cleaning, corner stress, target-market requirements, and whether the cooler will contain condensation, spills, or loose ice.
How do you make a cooler bag leak resistant?
Leak resistance depends on the liner material, seam construction, corner design, zipper position, and transitions between panels. Using a water-resistant outer fabric alone does not prevent liquid from escaping through stitched liner seams or openings. For many lunch bags, controlling condensation and minor spills is sufficient, while products designed for loose ice need a more demanding liner and seam system. A defined leakage test using a known volume, duration, and inspection method should be completed before making strong performance claims.
How is custom cooler bag capacity calculated?
For a rectangular interior, theoretical capacity can be estimated by multiplying internal length, width, and height and converting the result to liters. Actual usable capacity will usually be lower because corners, seams, liner folds, zipper geometry, foam, and structural components occupy space. The most reliable approach combines volume calculation with real loading. Place the intended bottles, cans, meal boxes, or delivery containers inside the sample and confirm that users can insert, remove, and arrange them comfortably.
How long does it take to develop a custom cooler bag sample?
A conventional sewn cooler bag sample may often require roughly 5–15 working days once dimensions, materials, insulation, lining, logo, and main structural details are sufficiently clear. Simple revisions can sometimes be completed more quickly, while molded EVA parts, special materials, custom webbing, unusual zipper systems, complex printing, or custom retail packaging can extend the development period. Actual timing should be confirmed after the manufacturer reviews the final specifications and material availability.
What should be approved before custom cooler bag bulk production?
Before bulk production, approve the final physical sample, pattern version, bill of materials, fabric, liner, foam type and thickness, webbing, zipper, hardware, logo artwork, logo location, dimensions, colors, labels, packaging, carton marks, and important inspection points. These records become the production standard. Clear approval is particularly important for repeat orders because it allows future production to reproduce the same product without depending on verbal instructions or someone remembering how the original sample was made.


