 Skip to content

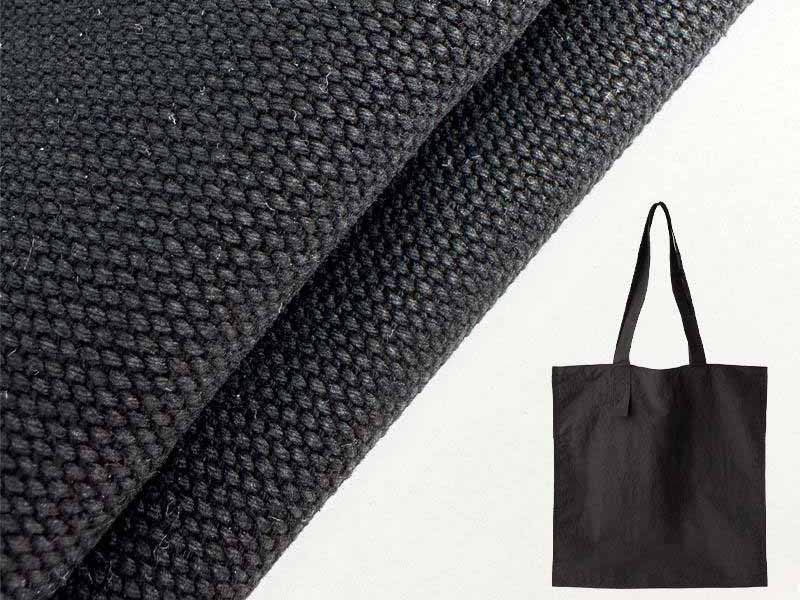
Choosing tote bag fabric looks simple until a real product moves from a drawing into sampling. A designer may specify “cotton canvas,” approve the color on a screen, and expect the finished tote to feel substantial. Then the first sample arrives and feels too soft, the logo sinks into a coarse weave, the handles distort the top edge, or the bag becomes much heavier than expected once the fabric, lining, pockets, and hardware are combined. These are not unusual production problems. They usually come from selecting material by name rather than by how the finished tote needs to perform.
For most tote bag projects, the right fabric is the material that matches the intended load, structure, appearance, branding method, maintenance needs, cost target, and sales environment. Cotton works well for soft and lightweight applications, canvas adds body and durability, while polyester and nylon can offer lower weight, easier cleaning, abrasion resistance, and functional coatings. GSM or ounce weight should always be considered together with weave, finish, construction, reinforcement, and testing rather than treated as a quality score on its own.
A useful way to think about tote bag fabric is to imagine two products that look almost identical in a sketch. One is used as premium packaging for skincare products and may carry less than 2 kg. The other is sold in a bookstore and may regularly carry several heavy books. Both could technically be made from cotton, canvas, or polyester, but the correct specification will be different. The rest of this guide explains how to make that decision in a way that works not only on a material swatch, but also in sampling, bulk production, retail use, and repeat orders.
What Should You Define Before Choosing Tote Bag Fabric?

Choosing tote bag fabric should begin with the finished product rather than a fabric catalog. Define what the tote will carry, where it will be used, how structured or foldable it should feel, what branding process will be applied, and what commercial position it needs to reach. These decisions provide a much more reliable basis for selecting fiber, weave, GSM, finish, reinforcement, and construction than choosing a material only because it looks attractive.
What Will the Tote Carry?
The contents of the tote should be one of the first things discussed during product development because they determine where stress will occur. A conference bag carrying brochures experiences relatively light and evenly distributed loads, while a grocery tote may carry bottles, cans, packaged food, or other items that concentrate force at the bottom corners. A bookstore tote can face repeated high loads from rigid books, while a beauty or gift tote may carry lighter products but need better shape retention and a cleaner presentation.
The most useful specification is therefore not an impressive maximum-load statement but a realistic working load. A lightweight promotional tote might normally carry less than 2–3 kg, while a reusable shopping or bookstore tote can easily be expected to handle 5–10 kg depending on its dimensions and intended use. These figures are development references rather than universal ratings because the fabric is only one part of the structure. Handles, stitch type, seam allowance, bartacks, reinforcement layers, gussets, thread, and construction quality all influence the completed bag.
In practical use, a tote often fails first at the handle attachment, bottom seam, gusset corner, or stitch line rather than through the middle of the fabric panel. That is why simply increasing canvas weight does not automatically create a stronger finished product. A well-designed medium-weight material with properly reinforced handle roots can outperform a heavier fabric that is poorly constructed. A good development brief should therefore record the expected carrying load together with the handle type, handle drop, bag size, gusset depth, reinforcement plan, lining requirement, and frequency of use.
For projects intended for repeated use, it is also useful to consider how the contents move while the tote is being carried. A rigid laptop can repeatedly rub against the same internal corner, while bottles may push outward against a gusset. Books can create concentrated pressure along the bottom seam. These patterns help determine whether the product needs a denser weave, stronger lining, bottom reinforcement, wider handles, or a different seam construction rather than simply more fabric weight.
Where Will the Tote Be Used?
Usage environment changes what counts as a good material. A tote used as retail packaging may need to look clean, feel pleasant, carry a few products, fold into a compact carton, and print well. A beach tote needs to tolerate sand, moisture, repeated handling, and rough surfaces. A bookstore tote needs stronger abrasion resistance at the bottom and corners. A fashion tote may prioritize drape, washed texture, color, and surface character more than maximum strength.
The sales environment also affects material choice. A customer touching a tote in a physical store immediately notices whether the fabric feels thin, stiff, soft, coarse, or substantial. A 120 GSM cotton bag and a 350 GSM canvas bag may perform the same basic carrying function, but they communicate completely different levels of perceived value. For a promotional event, the lighter version may be exactly right. For a paid retail product, it may feel under-specified.
Outdoor exposure introduces another set of questions. If the tote may encounter occasional rain, coated polyester or treated canvas may be more appropriate than untreated cotton. If it will be stored in vehicles, dragged across floors, or used during travel, abrasion resistance may become more important than softness. For products expected to be washed, shrinkage, colorfastness, print durability, and care instructions become part of the material decision before sampling begins.
The goal is not to add technical features for the sake of sounding premium. A heavily coated synthetic fabric would be unnecessary for an indoor gift tote that will only carry boxed products. At the same time, untreated lightweight cotton may be a weak choice for a reusable outdoor tote expected to see moisture and frequent cleaning. Good material selection comes from matching performance to the actual environment instead of choosing the most technical option available.
What Should the Finished Tote Feel Like?
Hand feel is one of the hardest characteristics to communicate in a specification sheet, yet it strongly affects how the finished tote is perceived. Terms such as “premium,” “soft,” “natural,” “structured,” and “heavy-duty” are useful for describing a direction, but they are not measurable standards. Two fabrics with similar fiber content and GSM can feel very different because of yarn size, weave density, washing, coating, surface finishing, and stiffness.
A medium washed canvas can feel more refined than a very heavy untreated canvas because it has a softer, more relaxed hand. A lightweight high-density polyester can feel cleaner and more sophisticated than a heavier low-density synthetic fabric. A natural cotton tote may feel casual and environmentally conscious even though it has less structure than a coated polyester product. The right hand feel depends on what the brand wants customers to experience.
| Desired Tote Character | Typical Fabric Direction | Common Working Range | Main Consideration |
|---|---|---|---|
| Soft and foldable | Cotton | 100–180 GSM | Compact packing and casual use |
| Natural retail feel | Cotton / light canvas | 180–280 GSM | Printability and touch |
| Structured lifestyle tote | Canvas | 280–420 GSM | Shape retention |
| Heavy premium tote | Dense canvas | 420–600+ GSM | Bulk, sewing and freight |
| Lightweight functional tote | Polyester / nylon | 150–300 GSM equivalent range | Coating and abrasion performance |
| Rustic gift tote | Jute / jute blend | Varies by weave | Texture and print limitations |
These ranges should be treated as practical development references rather than strict industry classifications. A tightly woven 280 GSM canvas can feel firmer than a loosely woven 330 GSM fabric, and finishing can change both drape and perceived thickness. Tote dimensions also matter. A fabric that feels stable on a small 30 × 35 cm bag may feel much softer on a wide 50 × 40 × 15 cm design because the larger panels have more room to bend and collapse.
What Cost and Order Goals Matter?
Fabric price per meter is only one part of tote bag cost. A heavier material can increase fabric consumption by weight, but it may also influence sewing speed, needle selection, seam handling, packing density, carton weight, and freight. A coated fabric may cost more to print or require additional testing. A thin material may look economical at first but later need lining, interfacing, or reinforcement to achieve the required appearance and strength.
For larger orders, small differences become meaningful. An $0.08 increase in finished cost becomes $800 across 10,000 pieces. That difference may be entirely justified if the better fabric eliminates an additional backing layer, reduces printing problems, or improves repeat-order consistency. Conversely, specifying an unnecessarily heavy canvas may add material and freight cost without creating a noticeable improvement for the end user.
A useful total-cost review should include the main fabric, usable width, cutting efficiency, dyeing, washing, coating, printing, embroidery, lining, reinforcement, sewing time, packaging size, pieces per carton, shipment weight, inspection requirements, expected rejection risk, and repeat-order availability. This approach gives a more realistic picture than comparing two fabric quotations side by side.
Material availability should also be considered when a product is expected to remain in the market for several seasons. A fabric that is easy to source consistently may have more commercial value than a slightly cheaper option that changes frequently between mills or production lots. For long-term product lines, repeatability in color, hand feel, weight, and finish can save considerable development time when the next order is placed.
Which Fabrics Work Best for Tote Bags?

There is no single fabric that is best for every tote bag. Cotton suits soft, lightweight, and highly printable designs; canvas works well where additional body and repeated use are important; polyester and nylon support lighter and more functional designs; jute creates a coarse natural character; and recycled materials can support specific sourcing goals. The correct choice depends on how the product will be used, decorated, maintained, priced, and reproduced over time.
Is Cotton Right for Lightweight Totes?
Cotton remains one of the most common tote bag materials because it feels familiar, folds easily, accepts many printing processes, and works well for simple constructions. It can be dyed, washed, bleached, left natural, or produced with recycled fiber content depending on the product direction. For events, retail packaging, gift-with-purchase programs, promotional campaigns, book launches, and lightweight merchandise, cotton often provides a useful balance between appearance, cost, and customization.
The term “cotton tote,” however, covers a very wide range of materials. A 100–120 GSM cotton bag can feel thin, flexible, and easy to fold, while a 200–250 GSM cotton bag feels substantially more solid. Both may be made from cotton, but they do not serve the same market position. Lightweight cotton is useful when compact packing and low material consumption are priorities, but it may become translucent, wrinkle more easily, and show the shape of the contents.
Around 150–220 GSM, cotton typically begins to feel more suitable for branded merchandise and reusable packaging while still remaining softer and easier to fold than heavy canvas. This range is often a practical starting point when a product needs better perceived quality without becoming highly structured. The actual result will still depend on weave, yarn, finishing, and bag dimensions.
Cotton also requires realistic care planning. Natural fiber can shrink when washed, particularly if it has not been pre-shrunk or finished for dimensional stability. Dark shades may need colorfastness checks, and natural unbleached cotton can vary slightly in tone between production lots. For repeat programs, approving a physical swatch, weight, finish, and color reference is much more reliable than specifying only “natural cotton.”
When Is Canvas the Better Choice?
Canvas becomes attractive when the tote needs more structure, higher perceived durability, and a more substantial hand feel. It is frequently used for bookstore bags, reusable grocery totes, lifestyle products, fashion merchandise, wine carriers, corporate merchandise, premium promotional bags, and retail products that are expected to remain in use for months rather than one event.
It is important to understand that canvas and cotton are not always opposing material categories. Cotton describes the fiber, while canvas describes a dense woven construction. Many tote bags described as canvas are actually made from cotton canvas. This distinction matters because “cotton versus canvas” can otherwise create confusion during sourcing. A lightweight plain-woven cotton and a dense cotton canvas may use the same fiber but behave very differently.
Canvas is particularly useful when the tote includes gussets, internal pockets, external pockets, reinforced handles, embroidery, leather or PU patches, zippers, snaps, rivets, or bottom panels. Its denser construction can provide better support for these features and make the finished product feel more substantial. Medium canvas in roughly the 280–400 GSM range often works well for reusable retail and lifestyle products, while heavier constructions above approximately 400 GSM can create much more noticeable body.
Heavier canvas should still have a clear purpose. Thick materials create bulky seam intersections, require stronger needles and suitable sewing machines, increase finished weight, occupy more carton volume, and can make a tote feel unnecessarily rigid. Choosing 16 oz canvas when 10–12 oz already meets the required function may add cost without improving the user experience. The best specification is the weight and construction that gives the finished tote enough strength and shape without unnecessary material.
Do Polyester and Nylon Fit Functional Totes?
Polyester and nylon are valuable alternatives when a tote needs low weight, easier cleaning, abrasion resistance, bright colors, coatings, or a more technical appearance. They are widely used in sports, travel, event, outdoor, foldable, and functional bag categories where natural texture is less important than repeatable performance.
Synthetic materials are often described using denier, such as 210D, 300D, 420D, or 600D, rather than only GSM. Denier refers to yarn linear density, so it should not be treated as the same measurement as finished fabric weight. A 600D polyester cannot be directly compared with a 300 GSM canvas simply because one number is larger. The weave, coating, yarn construction, and finished GSM still need to be understood.
Polyester is commonly selected for products requiring good color options, print compatibility, water-resistant coatings, easy wiping, and relatively low moisture absorption. Nylon can be attractive where softer technical hand feel and abrasion performance are priorities. In travel-oriented or outdoor-inspired products, these characteristics can make the finished tote feel more appropriate than cotton or canvas.
Coating makes a major difference. Uncoated polyester, PU-coated polyester, and PVC-backed polyester can differ significantly in stiffness, odor, water resistance, sewing behavior, heat sensitivity, and print adhesion. A complete material specification should therefore record denier, weave, finished weight, coating type, finish, color, and any performance requirements rather than simply describing the product as a “600D polyester tote.”
Are Jute and Recycled Fabrics Good Options?
Jute is useful when its rough natural texture is part of the visual identity of the tote. It is common in wine bags, grocery programs, gift packaging, garden-related products, and lifestyle collections that intentionally want a rustic look. Its coarse weave gives it a distinctive appearance, but that same texture affects printing, cutting, and edge finishing.
Fine text and thin graphic lines may lose definition on open or uneven jute surfaces, so artwork needs to be evaluated on the actual material. Jute can also fray more aggressively than tightly woven cotton or polyester, making seam construction and binding important. For premium applications, blends or laminated constructions are sometimes used to improve stability while retaining the natural surface appearance.
Recycled cotton and rPET fabrics can support sustainability-focused product programs, but “recycled” is not a complete specification. Recycled material still needs to be evaluated for composition, GSM, weave, strength, surface character, printability, color consistency, availability, and documentation. A recycled-content claim should be tied to the actual material used for the order rather than treated as a general marketing statement.
For established brands, documentation becomes especially important because a certified material does not automatically mean that every finished tote carries the same certification. Material certification, project-specific testing, and finished-product requirements should be kept separate and clearly documented. This distinction is consistent with Lovrix’s documented compliance approach, which separates certified material options from finished-product certification and project-specific reports.
How Do GSM, Oz, Weave, and Finish Affect Performance?

GSM and ounces describe fabric mass per area, but they do not describe total quality. Higher fabric weight usually creates more body and material mass, while weave density, fiber type, yarn construction, washing, coating, and finishing determine how that mass behaves. Two fabrics with the same GSM can feel and perform differently, so weight should be treated as one specification within a larger material system.
What GSM or Oz Should You Choose?
GSM means grams per square meter and is widely used to describe textile weight. Canvas is also frequently sold in ounces per square yard. The mathematical conversion is approximately 1 oz/yd² = 33.9 GSM, which means an 8 oz fabric is theoretically around 271 GSM and a 12 oz fabric around 407 GSM. In commercial sourcing, quoted values may not always convert perfectly because suppliers can use nominal categories or measure fabric before or after specific finishing processes.
| Canvas Weight | Approx. GSM | Common Tote Direction | Typical Character |
|---|---|---|---|
| 6 oz | ~203 GSM | Lightweight merchandise | Flexible |
| 8 oz | ~271 GSM | Everyday reusable tote | Medium-light body |
| 10 oz | ~339 GSM | Retail / lifestyle tote | Noticeable structure |
| 12 oz | ~407 GSM | Premium reusable tote | Stronger body |
| 14 oz | ~475 GSM | Heavy lifestyle tote | Firm |
| 16 oz | ~542 GSM | Heavy-duty tote | Very substantial |
These values are conversion references rather than strict quality grades. A tightly woven 300 GSM fabric can sometimes feel more structured than a loosely woven fabric with a higher nominal weight. For that reason, swatches should be compared physically rather than selected from numbers alone.
Bag size changes how weight feels in the finished product. A 300 GSM canvas may provide excellent shape on a compact tote but feel softer on a very large shopper with deep gussets. Larger panels have more room to flex and deform, so dimensions should always be considered when determining whether additional weight or reinforcement is necessary.
Fabric weight also affects manufacturing and logistics. Heavier material changes needle requirements, seam thickness, folding volume, carton weight, and sometimes embroidery behavior. A useful material decision therefore asks not only whether the fabric feels substantial enough, but also whether the extra weight creates real value for the finished tote.
How Does Weave Affect Tote Structure?
Weave controls how yarns are arranged and therefore has a significant influence on opacity, surface smoothness, stiffness, stretching, abrasion, fraying, printing, and shape retention. Two materials with identical GSM can behave quite differently because one may use thicker yarns in a more open construction while the other uses finer yarns packed into a dense weave.
A dense construction usually produces a more stable cutting edge and a smoother surface for detailed printing. A more open weave can create attractive natural texture but may distort more easily under load and show more visible texture through printed areas. This can be desirable for a handmade or rustic look but less suitable for fine text, small logos, or precise graphics.
During fabric approval, practical checks should include warp and weft appearance, yarn thickness, light transmission, stretch by hand, fraying at cut edges, recovery after folding, surface smoothness, and how the material responds to a needle. These simple observations often reveal differences that are not visible in a basic GSM report.
Weave consistency matters especially in repeat orders. If a supplier changes yarn count or construction while keeping the fabric within approximately the same GSM range, the finished tote may technically meet the weight requirement but no longer match the approved sample. For long-term programs, the approved material record should therefore include not only weight and color but also a supplier reference, construction description, finish, and physical swatch.
Do Fabric Finishes Change Performance?
Finishing can transform the same base fabric into a very different product. Washed canvas becomes softer, more relaxed, and often more suitable for lifestyle products. Enzyme washing can reduce stiffness and create a worn-in appearance. Pre-shrinking can improve dimensional stability, while waxed treatments change surface feel, color depth, and moisture behavior.
Synthetic fabrics can receive PU, PVC, acrylic, or other coatings depending on their intended use. These treatments may alter water resistance, stiffness, surface friction, heat response, print adhesion, odor, fold marks, and the visibility of needle holes. A polyester fabric that prints well without coating may behave differently after a heavy PU finish has been added.
Finishing must therefore be considered together with branding. Heat transfer can affect coated materials, while screen-print adhesion can vary from one surface treatment to another. A waxed or heavily washed canvas may produce a visual effect that is attractive for a lifestyle brand but unsuitable for very precise graphics.
The safest approach is to treat finishing as part of the material specification rather than an optional cosmetic detail. The production swatch used for logo trials should match the actual finish intended for bulk production because testing an untreated fabric and later ordering a coated or washed version can produce very different results.
Is Heavier Fabric Always Better?
Heavier fabric is not automatically better. It is better only when the tote genuinely benefits from additional mass, stiffness, and structure. Increasing weight to solve every quality concern can create new problems in sewing, packing, freight, and user comfort without addressing the real structural weakness.
Moving from 300 GSM to 500 GSM increases fabric mass by about 67% per square meter, but it does not make the completed bag 67% stronger. If the handle attachment, seam construction, or reinforcement remains unchanged, those areas may still become the first point of failure. Strength needs to be evaluated at product level rather than inferred from fabric weight alone.
Very heavy materials also create bulky intersections where multiple layers meet. Bottom corners, top hems, handle roots, and gusset seams can become difficult to turn and sew cleanly. Extra stiffness may reduce foldability and make a tote feel uncomfortable against the body. Packaging density can also decline because fewer finished bags fit into each carton.
A better objective is to choose the lightest material that reliably achieves the required structure, durability, appearance, branding performance, and positioning with an appropriate safety margin. That approach reduces unnecessary cost while keeping the finished product aligned with what the user actually needs.
Which Fabric Is Best for Printing and Branding?

Fabric and branding should be selected together because surface texture, fiber, coating, color, GSM, logo size, and heat sensitivity all affect decoration quality. Cotton and canvas suit many screen-printing applications, polyester can work well with transfer-based techniques, and embroidery requires enough stability to resist distortion. Patches, woven labels, rubber badges, and metal plates also introduce specific reinforcement and attachment requirements.
Which Fabrics Suit Screen Printing?
Screen printing remains one of the most practical tote bag decoration methods because it handles logos, text, and simple graphics efficiently across medium and larger production quantities. Cotton and canvas are frequently selected because suitable untreated surfaces generally accept textile inks well and provide a familiar printed appearance.
Surface texture still matters. Fine lines and small type reproduce more cleanly on smoother, denser fabric than on coarse canvas or jute. Dark fabric may require an underbase before the final color is printed, while large solid print areas can make the surface feel noticeably stiffer. The appearance of the same Pantone color can also change depending on whether it is printed on natural cotton, optical white cotton, black canvas, or colored polyester.
Placement should be considered while the pattern is being developed. Printing too close to a side seam, bottom gusset, zipper, pocket, or handle root can create uneven screen contact and inconsistent results. The flat printable area needs to be understood before sewing, particularly for large logos or graphics.
For production approval, the specification should identify artwork size, print position, color reference, method, and accepted appearance on the actual fabric. Digital mockups are useful for communication, but a physical printed panel or finished sample provides far better evidence of whether the design works on the chosen material.
When Should You Use Heat Transfer or Digital Printing?
Heat transfer becomes useful when artwork contains gradients, photographs, many colors, or fine details that would require numerous screen setups. It is commonly used on polyester and other compatible surfaces, although the exact pressing temperature, adhesive, dwell time, and pressure depend on both the transfer system and fabric construction.
Heat-sensitive surfaces can develop gloss marks, soften, distort, or show dye migration. Coatings can also react differently from uncoated base material. For that reason, production settings should be established on the actual fabric rather than copied from another tote style that only looks similar.
Digital printing can be useful for fashion-oriented products, complex graphics, smaller production runs, and designs where visual differentiation is more important than achieving the lowest possible decoration cost. All-over printed products require more planning because artwork placement can shift around seams, gussets, and cut panels.
The simplest way to choose between methods is to start with the artwork and material together. A three-color logo on natural cotton may be ideal for screen printing, while a photographic image on polyester may suit transfer or sublimation. A full-surface fashion pattern may justify printed yardage before cutting. No printing method is universally superior across every material and design.
Is Embroidery Suitable for the Fabric?
Embroidery adds texture and perceived value, particularly on medium and heavier canvas, Oxford, and other stable woven materials. Its main technical challenge is that every stitch creates localized tension. If the fabric is lightweight or the artwork is very dense, the panel can pucker, pull inward, or become stiff unless backing, stitch density, and digitizing are carefully controlled.
Lightweight cotton can still be embroidered, but the design usually requires more attention to stabilizer, logo dimensions, thread density, and placement. A large dense embroidered graphic may contain thousands of stitches in a relatively small area, which can significantly change the behavior of a thin fabric panel.
Embroidery also influences production sequence. Panels are often embroidered before the tote is fully assembled so that they can lie flat in the embroidery frame. If the bag has a lining, the lining can conceal backing and reverse stitches. On an unlined tote, the backside finish becomes part of the visible product quality.
For premium products, embroidery can create a stronger tactile identity than flat printing, but it should be chosen because it matches the product and fabric rather than because it is automatically assumed to be more premium. The final decision should be based on an embroidery trial on the exact production fabric.
Do Patches and Labels Need Different Fabrics?
Patches, woven labels, rubber badges, silicone badges, leather or PU patches, and metal plates can extend branding beyond direct printing, but each method introduces different mechanical demands. A lightweight cotton body may sag under a heavy metal plate, while a thick rubber patch can distort a soft fabric unless the mounting area is reinforced.
Woven labels are generally easy to integrate into seams or apply to a broad range of fabrics. Leather or PU patches work well with lifestyle and canvas products but require attention to wash behavior and edge finishing. Rubber and silicone patches suit outdoor, sports, and technical products but add localized weight. Metal plates can create a polished appearance but normally require secure backing or hardware attachment.
Branding decisions should therefore be made before construction is finalized. The location of a metal plate may require an internal reinforcement patch. Embroidery may influence whether a lining is needed. A large woven label may change seam allowance or pocket placement.
This integrated approach reflects established manufacturing practice: logo methods should be matched to the material and use condition rather than applied as interchangeable decoration options. Lovrix’s documented capabilities similarly distinguish between screen printing, transfer, digital printing, embroidery, woven labels, leather patches, rubber badges, metal plates, and other branding processes based on material suitability.
How Do Durability, Care, and Cost Affect the Choice?
Tote durability depends on the complete construction rather than fabric weight alone. Fabric strength, abrasion resistance, seam design, handle attachment, reinforcement, coating, washing behavior, and the actual load carried all influence service life. Cost should therefore be evaluated across fabric, construction, branding, packaging, testing, freight, and repeat-order consistency rather than comparing only the price per meter.
How Much Load Must the Tote Handle?
Load-bearing performance is often misunderstood because it is easy to focus on fabric strength while ignoring the rest of the product. A 300 GSM canvas may appear strong enough for a heavy reusable tote, but the completed bag still contains multiple potential weak points at the handles, seams, gussets, top hem, stitch holes, and reinforcement areas.
Force moves through the bag as a system. Contents press against the bottom panel, that force travels into the side seams and gusset, and the entire load eventually transfers through the handle attachment points. If a narrow handle is attached close to the top edge with limited stitch area, that connection can fail even when the main fabric remains undamaged.
For repeated-use products, testing the finished sample provides more useful information than estimating capacity from fabric GSM. If the tote is expected to carry around 6 kg in normal use, the development team can test the completed sample around the intended working condition and apply an appropriate safety margin based on project requirements.
Repeated loading also matters. A product that survives one dramatic static test may still loosen after hundreds of carrying cycles. For reusable totes, repeated lift testing and inspection of stitch holes, handle roots, and seam distortion can reveal problems that a single maximum-load test will not show.
Is Abrasion Resistance Important?
Abrasion becomes important whenever a tote is intended for repeated use. Wear tends to appear at the bottom corners, lower side panels, handle surfaces, seam edges, and areas that repeatedly contact clothing, floors, counters, shopping carts, vehicle interiors, or other bags.
A grocery tote may be placed on rough surfaces dozens of times in a month. A commuter tote rubs against clothing while walking. A travel tote may be pushed under seats or stacked with luggage. The center of the fabric panel can remain in excellent condition while the corners and bottom show visible wear much earlier.
Material aging can also be part of the design. A washed canvas may gradually soften and develop a worn appearance that suits a casual lifestyle product. The same visual change would be undesirable on a clean corporate tote intended to retain a formal appearance. Durability therefore includes both physical survival and how the material looks as it ages.
For projects where abrasion is a serious risk, fabric testing and finished-product use trials can provide better information than descriptive terms such as “heavy-duty.” Lovrix’s documented testing approach includes abrasion resistance, seam strength, load-bearing verification, print rubbing, coating adhesion, and related checks selected according to product use and risk.
Does the Tote Need Water Resistance?
Water resistance should begin with a clear use scenario. A tote that only needs to survive occasional light rain does not require the same construction as a product designed to carry wet clothing, protect electronics, or remain outdoors for extended periods.
A coated polyester or nylon fabric may resist water effectively at the material level, but ordinary stitched seams still contain needle holes. Water can also enter through an open top, zipper, binding, side seam, hardware attachment, or bottom construction. For this reason, a water-resistant fabric does not automatically create a waterproof finished tote.
Care requirements should be treated with the same precision. A cotton tote may be washable, but washing can cause shrinkage, color change, or surface softening. Coated fabrics can delaminate under unsuitable conditions. Heat-transfer graphics may react differently from screen prints, while metal hardware can corrode if the finish is not appropriate.
A finished-product care test is more reliable than assuming the main fabric determines the entire washing instruction. Fabric, print, embroidery, reinforcement, lining, coating, thread, and hardware should all be compatible with the recommended care method before the instruction is printed on a label.
How Does Fabric Choice Affect Total Cost?
Material selection affects many cost layers beyond the basic fabric quotation. A cheaper canvas that frays heavily may require more binding or slower sewing. A thinner cotton may need lining or reinforcement to achieve the required appearance. A coated polyester may require a specialized logo process. A heavy canvas may increase shipment weight and reduce the number of pieces that fit into each carton.
| Cost Layer | Questions to Check |
|---|---|
| Fabric | Price, width, consumption, waste, dyeing and finishing |
| Construction | Sewing time, seam bulk and reinforcement |
| Branding | Screens, transfer, embroidery, patches and hardware |
| Components | Lining, snaps, zippers, labels and webbing |
| Testing | Material and finished-product verification |
| Packaging | Folding size, individual packing and carton capacity |
| Logistics | Carton weight, pieces per carton and freight |
| Quality Risk | Rework, rejects, complaints and returns |
| Repeat Orders | Material availability and batch consistency |
The financial impact becomes clearer at larger volumes. A material that adds $0.10 to the finished tote adds $1,000 across 10,000 pieces, but the extra cost may be justified if it removes a separate reinforcement component, reduces rejects, or creates a noticeably better retail product. At the same time, adding $0.10 for a heavier specification that customers cannot perceive may simply reduce margin.
For long-term programs, consistency also has economic value. A fabric that remains available, colors reliably, prints predictably, and matches previous batches can reduce development time and approval costs on repeat orders. Total product economics therefore include future operational efficiency, not just the price of the first production run.
How Should You Validate Fabric Before Bulk Production?
Tote bag fabric should be validated through physical swatches, branding trials, a completed prototype, and relevant performance checks before bulk production begins. Once approved, the material composition, GSM, color, finish, supplier reference, construction, logo method, packaging, and inspection requirements should be recorded so production can be measured against a defined standard rather than subjective memory.
Do You Need Fabric Swatches First?
A physical swatch is one of the simplest ways to prevent expensive misunderstandings. Photographs and digital renderings cannot accurately communicate thickness, surface friction, stiffness, yarn texture, opacity, drape, stretch, coating feel, or how the material changes under different lighting.
A supplier may describe a material as “12 oz washed canvas,” but that phrase alone does not explain whether the fabric feels crisp, soft, heavily washed, coarse, dense, dry, or slightly fuzzy. Those characteristics become important when the tote is expected to represent a specific retail position.
Swatch review should cover weight, hand feel, stiffness, weave density, opacity, shade, folding behavior, edge fraying, coating, backside appearance, and suitability for the planned logo process. For color-sensitive programs, viewing the material under daylight and indoor lighting is useful because beige, olive, gray, and other muted colors can shift noticeably under different light sources.
For branding projects, a blank swatch is not enough. Screen printing, heat transfer, embroidery, or a patch should be tested on the production material whenever the logo result is commercially important. Once approved, the swatch should be labeled with material code, composition, nominal GSM, color reference, finish, supplier, and approval date so it can be used again during bulk production and repeat orders.
Should You Make a Tote Bag Prototype?
A swatch confirms the fabric, while a prototype confirms whether the entire product works. Sewing changes how material behaves because multiple layers are folded, joined, reinforced, tensioned, and shaped. A fabric that feels perfect when flat may become too bulky at a gusset corner or too soft once used across a very large panel.
The prototype should be tested in the same way the customer is expected to use the product. Load it with realistic contents, carry it by hand, place it on a shoulder, set it on the floor, open the pockets, test any closure, and fold it if compact storage is part of the design. These simple actions reveal usability problems that are difficult to see on drawings.
Finished dimensions should also be checked carefully. Width, height, gusset depth, handle drop, handle spacing, pocket position, opening width, and logo placement all influence use. A handle drop of 20 cm and one of 30 cm may both look acceptable on a drawing, yet one may function mainly as hand carry while the other fits more comfortably over a coat.
Sampling should therefore be treated as functional verification rather than only visual approval. The purpose is to find where material, structure, proportion, branding, and use do not align while changes are still relatively inexpensive.
Which Fabric Tests Matter?
Not every tote needs the same level of testing. The test plan should match product function, sales channel, risk, material construction, and the consequences of failure. A basic conference tote may only require appearance inspection, dimensions, GSM checking, printing approval, and basic seam verification, while a reusable retail tote designed for heavier loads may justify additional strength and abrasion checks.
Useful tests can include GSM measurement, fabric width, shrinkage, colorfastness, abrasion resistance, tear strength, tensile strength, seam strength, handle pull strength, static load, repeated load, print rubbing, embroidery durability, coating adhesion, and water-resistance testing. The goal is not to create the longest laboratory report possible but to verify the characteristics most likely to cause complaints, returns, or product failure.
For coated outdoor totes, coating adhesion and moisture behavior may be more important than washing performance. For printed promotional totes, logo rubbing and color consistency may deserve more attention than maximum load. For heavy bookstore or grocery totes, handle attachment and repeated carrying become more significant.
A disciplined manufacturer should also separate internal checks from third-party laboratory reports and avoid presenting every possible test as mandatory for every product. The most useful validation process is one that is proportionate to risk and produces evidence directly connected to the tote’s intended use.
How Do You Control Sample-to-Bulk Consistency?
An approved sample only becomes useful when its important characteristics are translated into records that production teams can follow. Relying on memory or descriptions such as “the same black 12 oz canvas as last time” leaves too much room for interpretation when material is reordered or production is repeated months later.
A practical approval package may include the physical sample, approved fabric swatch, material specification, BOM, color reference, logo artwork, logo placement dimensions, pattern version, measurement chart, stitch details, packaging requirements, inspection standards, and any relevant test results. Incoming material can then be compared with these references before cutting begins.
For important projects, incoming fabric inspection may include GSM, width, color, visible defects, hand feel, coating, and shrinkage where relevant. Textile dyeing works within tolerances, so repeat lots can show some variation. Defining what is acceptable is more realistic than expecting an undefined standard of “exactly identical.”
Traceability becomes particularly useful when multiple SKUs, colors, or production batches are involved. If the manufacturer can identify which fabric lot, color, pattern version, logo file, and approved sample belongs to each production run, quality issues can be isolated and corrected much more efficiently. Lovrix’s documented quality system similarly places material verification, GSM inspection, color checking, printing and embroidery inspection, in-line control, and final inspection at multiple stages rather than relying only on the final finished product.
Final Thoughts
Choosing tote bag fabric is ultimately a product-development decision rather than a simple choice between cotton, canvas, polyester, nylon, jute, or recycled material. The best fabric is the one that fits how the tote will actually be carried, how much structure it needs, how the brand will be applied, how the product will be cared for, what price level it needs to reach, and whether the same result can be reproduced reliably in bulk.
A useful process begins with end use and works backward. Define the load, dimensions, structure, hand feel, branding, care requirements, and commercial limits first. Then compare material composition, GSM or ounce weight, weave, finish, coating, and availability. Physical swatches narrow the options, a completed sample proves the construction, and appropriate testing verifies the areas that create real risk.
The most expensive material is not automatically the best, and the lightest fabric is not automatically the most economical. A well-specified medium-weight canvas can outperform an unnecessarily heavy one when the structure is engineered correctly. A synthetic fabric may be a better fit than natural cotton when cleaning or moisture resistance matters. A lightweight cotton can be exactly the right solution for retail packaging when it is not expected to behave like a grocery bag.
When a tote project is still at the sketch, reference-image, existing-sample, or early material-selection stage, that is often the best time to involve an experienced manufacturing team. Material, handles, structure, printing, reinforcement, packaging, and quality standards are easier to optimize before the first sample is built than after a bulk order has already been approved. Lovrix’s material-driven development approach is built around that sequence: evaluate the material and structure first, verify the sample, and then convert the approved product into a repeatable production standard.
Frequently Asked Questions
What is the best fabric for a tote bag?
There is no single best tote bag fabric because the correct choice depends on use. Lightweight cotton works well for promotional and retail packaging, canvas is better when the tote needs more structure and repeated use, while polyester and nylon can be more suitable for lightweight, functional, easy-clean, or water-resistant applications. Jute works well when coarse natural texture is part of the design. The final choice should consider load, bag size, GSM, weave, branding, care, cost, and the required product life.
What GSM is best for a tote bag?
A practical starting range is around 100–180 GSM for lightweight cotton totes, 180–280 GSM for more substantial cotton or light canvas products, 280–420 GSM for structured reusable canvas totes, and approximately 420–600+ GSM for heavier canvas designs. These ranges are not fixed standards. A tightly woven 300 GSM material can feel firmer than a loosely woven fabric at a higher weight, so GSM should always be evaluated together with weave, finish, tote dimensions, reinforcement, and a finished sample.
Is 12 oz canvas good for tote bags?
A 12 oz canvas is approximately 407 GSM by mathematical conversion and is commonly suitable for substantial reusable, retail, lifestyle, and premium tote designs. It provides noticeably more structure than lighter 6–8 oz canvas, but it is not automatically necessary for every product. Smaller or lightly loaded totes may perform well with a lower weight, while large or heavily structured products may need additional reinforcement regardless of fabric weight. Sampling the actual tote remains the most reliable way to confirm whether 12 oz is appropriate.
Is cotton or canvas better for tote bags?
Neither is universally better, and the comparison can be misleading because many canvas fabrics are made from cotton. Cotton describes fiber content, while canvas generally describes a denser woven construction. Lightweight plain cotton is usually softer, easier to fold, and suitable for promotional or simple retail applications. Cotton canvas offers more body and works better for reusable bags, embroidery, gussets, pockets, and heavier products. The decision should therefore compare actual fabric construction and weight rather than only the words “cotton” and “canvas.”
Is polyester good for reusable tote bags?
Polyester can be an excellent tote bag material when low weight, easy cleaning, bright colors, coating options, dimensional stability, or water resistance are important. It is widely used in sports, travel, promotional, outdoor, and foldable tote designs. Specifications such as 210D, 300D, 420D, or 600D describe yarn denier rather than finished fabric weight, so the complete material specification should also consider weave, finished GSM, coating, print method, and abrasion performance before production.
How do I choose fabric for a printed tote bag?
Choose the material and printing method together. Smooth cotton and canvas are commonly suitable for screen printing, while polyester may work well with heat transfer or sublimation depending on its construction and coating. Fine text and detailed graphics usually reproduce better on smoother surfaces than on coarse canvas or jute. Dark colors may require an underbase, coated materials may need adhesion testing, and logo placement should avoid bulky seams, gussets, and handle attachment points. A print trial on the actual production fabric should be approved before bulk manufacturing.
Should tote bag fabric be tested before mass production?
Testing is useful whenever material or construction failure could create meaningful quality problems. Depending on the project, checks may include GSM, shrinkage, colorfastness, abrasion resistance, seam strength, handle pull strength, repeated load, print rubbing, embroidery durability, coating adhesion, and water resistance. Not every tote needs every test. The most effective approach is to identify the product’s real risks, test the finished sample where possible, and use the approved material, sample, BOM, dimensions, and quality criteria as the reference for bulk production.


