 Skip to content

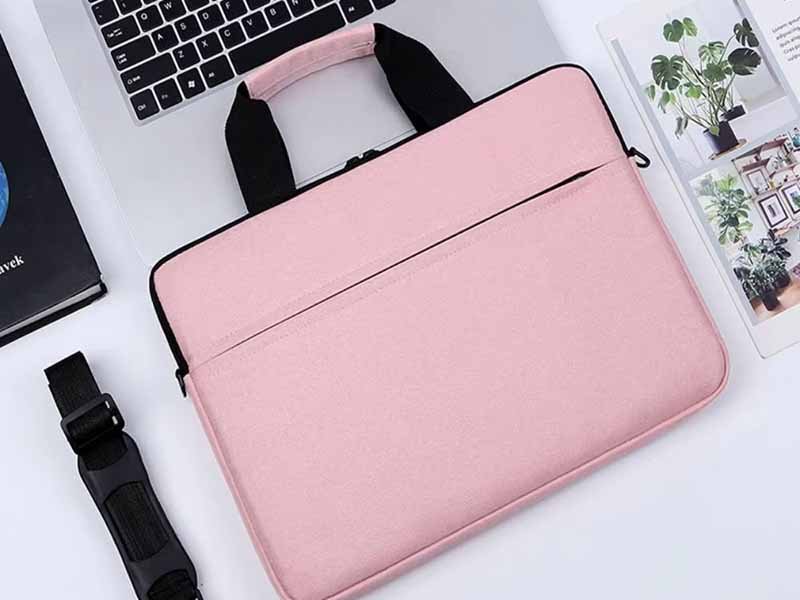
A laptop bag looks simple until a product team actually tries to manufacture one. A difference of several millimetres in a compartment can make a computer difficult to insert. Foam can look thick in a sample but still leave the bottom corners exposed. A shoulder strap can use strong webbing and still fail because the stitching or attachment patch is too weak. Even a visually impressive prototype can become a problem when the same construction must be repeated across thousands of units with consistent dimensions, materials and workmanship.
The best laptop bag manufacturer is therefore not simply the factory offering the lowest unit price. A strong manufacturing partner should understand device fit, padding, compartments, materials, straps, zippers, sampling, OEM/ODM development and bulk-production control. The right supplier should also be able to explain how an approved prototype becomes a repeatable production standard rather than relying on vague promises of “high quality.”
This is why comparing laptop bag manufacturers requires more than collecting quotations from twenty-five factories and choosing the cheapest offer. A corporate laptop sleeve, a premium leather briefcase and a 30-litre commuter backpack may all carry computers, but their material systems, structural risks and production methods are very different. The following guide looks at manufacturers from a sourcing and product-development perspective, helping you understand what to compare before a sample becomes an order and before an order becomes thousands of finished bags.
What Makes a Laptop Bag Manufacturer Worth Shortlisting?

A laptop bag manufacturer is worth shortlisting when it can demonstrate relevant product experience, accurate device-fit development, appropriate material selection, controlled sampling, OEM or ODM capability and reliable bulk-production management. Strong suppliers should explain how padding, compartments, straps, zippers, reinforcement and materials work together instead of using broad claims such as “premium,” “durable” or “shockproof” without supporting construction details.
Product-Specific Capability
Laptop bags are not ordinary backpacks with one extra pocket sewn into the lining. They carry relatively rigid, expensive and often heavy electronic devices, so the construction has to consider impact protection, weight distribution, access, comfort and repeated daily use. The first qualification question should therefore be whether the manufacturer has experience with the specific laptop product you are developing, rather than whether the factory has produced bags in general.
A close-fitting laptop sleeve demands accurate internal dimensions, edge protection and controlled foam thickness. A business briefcase puts more pressure on handles, hardware and structured panels. A messenger bag introduces cross-body load distribution and strap-hardware concerns, while a laptop backpack requires a much wider system involving shoulder straps, back padding, compartment position, zipper routes and overall balance. A travel backpack introduces still more variables because clothing, chargers, bottles and personal items may share the same structure with the computer.
Device dimensions should always be specified precisely. Commercial laptop programs commonly cover approximately 13-inch, 14-inch, 15.6-inch, 16-inch and 17.3-inch devices, but screen size alone does not define the outside dimensions of the computer. Two laptops sold as 16-inch machines can have noticeably different width, depth and thickness. A manufacturer should therefore work from real device measurements or a dimensional dummy rather than simply enlarging an existing 15.6-inch compartment.
Padding should also be evaluated as part of the full protection system. Several millimetres of foam may be appropriate for one structure, while another design requires additional bottom clearance, reinforced corners or a suspended compartment. More foam does not automatically create a safer product. Protection depends on where the material is placed, how it behaves under compression and whether hard accessories can press directly against the device during normal use.
Development and Sampling
The quality of a manufacturer often becomes visible before bulk production starts. A professional development team should be able to take a drawing, tech pack, reference photograph, existing sample or product concept and translate it into measurable construction requirements. That process normally involves pattern development, material selection, component confirmation, sample construction, fit checking and structured revisions rather than simply copying the exterior appearance of a reference bag.
A useful development brief should normally identify the exact laptop dimensions, expected accessory load, desired bag capacity, exterior material direction, lining, foam requirements, compartment structure, pocket layout, shoulder-strap or handle configuration, logo process, packaging expectations, target quantity and intended market position. Providing those details allows a capable factory to identify conflicts before cutting material rather than after the first sample has already been made.
The sample should then be evaluated under realistic loading conditions. Put the intended computer or a dimensional equivalent inside the compartment and add the charger, power bank, notebook, bottle, headphones and other items the user is expected to carry. Check whether the body changes shape, whether the zipper becomes difficult to close, whether hard objects press against the laptop and whether the bag remains comfortable after several minutes of actual carrying.
An approved prototype should eventually become a controlled production reference. Pattern versions, materials, foam, webbing, hardware, zipper specifications, logo placement and packaging should be documented rather than remembered informally. This matters because producing one attractive prototype is relatively easy compared with reproducing the same decisions consistently across 3,000 or 10,000 finished products.
For example, Lovrix’s documented product-development system includes laptop protection-layer design, internal compartment planning, shoulder-strap load distribution, handle reinforcement and sample-to-bulk structural control. These are the types of capabilities worth looking for when a laptop bag is being developed as a commercial product rather than purchased as a ready-made promotional item.
Commercial and Quality Fit
Technical competence does not automatically mean commercial compatibility. A factory designed around efficient 5,000-piece production programs may not be the most suitable partner for a 400-piece market test, while a small workshop that handles several hundred units comfortably may struggle with a retailer that requires tens of thousands of bags across repeated deliveries. Production scale, MOQ, communication and repeat-order management should therefore be evaluated together.
MOQ is more complicated than the number of finished bags the sewing factory agrees to produce. Fabric dyeing, custom webbing, zipper tape, molded buckles, branded hardware, printed packaging and special coatings can each have their own upstream minimums. A supplier might accept 500 finished bags but still require you to use stock fabric colors because the textile mill will not custom-dye the small quantity needed for five separate colorways.
Quality systems should also be evaluated through specific checkpoints rather than broad claims. Ask how materials are checked when they arrive, what happens during cutting and first-piece approval, whether production is inspected while sewing is still underway and how finished measurements, laptop fit, hardware, zippers, straps and packaging are checked before shipment.
| Area to Verify | Useful Evidence | Practical Check |
| Laptop fit | Approved sample or fit record | Test the actual device dimensions |
| Main material | Swatch and specification | Fiber, denier, coating and backing |
| Padding | Construction sample | Coverage, density and bottom clearance |
| Straps | Reinforcement sample | Bartacks, stitching and anchor area |
| Zippers | Component specification | Gauge, slider and opening path |
| Sampling | Revision record | Changes documented numerically |
| Bulk control | BOM and approved sample | Check material substitutions |
| QC | Inspection checklist | Incoming, in-line and final checks |
| MOQ | Written quotation | Confirm style and color minimums |
| Repeat orders | Version records | Confirm patterns and BOM are retained |
A manufacturer becomes much easier to evaluate once the discussion moves from general promises to evidence such as these. Factory size, website design and product photographs can support an initial impression, but they are not substitutes for understanding how the product is actually developed and controlled.
Which Are the 25 Best Laptop Bag Manufacturers?

There is no universal number-one laptop bag manufacturer because the most suitable factory depends on product type, materials, quantity, development complexity, target price and market position. The twenty-five manufacturers below represent different sourcing routes, including laptop specialists, backpack factories, neoprene specialists, leather manufacturers and broader OEM/ODM operations. They are best treated as manufacturers worth comparing rather than a fixed quality ranking.
25 Manufacturers to Compare
A useful manufacturer list should help a product team identify different production models rather than simply provide twenty-five company names. Some manufacturers are better aligned with technical commuter backpacks, some with corporate or promotional products, some with leather business cases and others with slim sleeves. The shortlist becomes useful only when those differences are compared against the specifications of the product being developed.
| Manufacturer | Main Base | Main Comparison Focus | Public MOQ Signal |
| Lovrix | Guangdong, China | Material and structure-led OEM/ODM | 500 pcs standard |
| Kingsons | China | Business and technology backpacks | Confirm by project |
| Fenglinwan | Dongguan, China | Laptop bags and sleeves | Confirm by project |
| YCT Bag | Jinhua, China | Laptop and business backpacks | Around 1,000 pcs |
| BUBM | Shenzhen, China | Laptop and electronics carry products | Confirm by project |
| Junyuan Bags | Fujian, China | Custom backpacks and bag programs | Confirm by project |
| KIVIN | Hunan, China | OEM/ODM backpacks | Around 500 pcs |
| Osgoodway | Fujian, China | Functional backpacks | Around 300–500 pcs |
| Panway | China | Travel, sports and laptop bags | Project-dependent |
| UMO VINA | Vietnam | OEM/ODM sewn bags | Project-dependent |
| Vancharli Outdoor | Asian production network | Business and outdoor bags | Project-dependent |
| ECO-ZY | Guangzhou, China | Custom and recycled-material bags | Around 200 pcs |
| Gentle Bags | Zhejiang, China | Custom laptop bags | Project-dependent |
| Uinta Design | Global manufacturing | Device-specific product development | Project-dependent |
| Ecophay | Shenzhen, China | Laptop work bags and sleeves | Project-dependent |
| EDIOM SPORTS | Guangdong, China | Neoprene laptop sleeves | Project-dependent |
| Mherder / BagsPlaza | Guangzhou, China | Leather laptop bags and sleeves | Product-dependent |
| Tamador | Guangzhou, China | Laptop and travel backpacks | Project-dependent |
| GenXport | International sourcing | Corporate laptop bag programs | Project-dependent |
| Ecobagfactory | Zhejiang, China | Promotional and custom laptop bags | Project-dependent |
| JU MEI Bags | Guangzhou, China | Laptop cases and sleeves | Project-dependent |
| Guangzhou Haoen Leather | Guangzhou, China | Business cases and laptop bags | Project-dependent |
| China Blooming Manufacture | China | Volume backpack production | Project-dependent |
| Xiamen Chuanghuasheng | Fujian, China | Mainstream backpack production | Project-dependent |
| Qingdao Bailiwei Bags | Qingdao, China | Backpack and travel programs | Project-dependent |
Lovrix is relevant when the development requirement extends beyond changing a logo on an existing catalogue item. Its documented standard custom-bag MOQ is 500 pieces per design, with the final requirement influenced by material availability, branding, packaging and structural complexity. The company supports both OEM projects based on drawings, samples and tech packs and ODM projects that begin with product concepts or reference images.
Kingsons has a strong public focus on technology-oriented and business backpacks. It is particularly relevant when laptop protection is combined with features such as business organization, trolley integration or anti-theft layouts. Manufacturers in this category can be attractive to brands selling through technology, travel or commuter channels, although product teams should still separate genuinely useful functions from features that add weight and cost without improving the end-user experience.
Fenglinwan focuses more directly on laptop bags, sleeves and protective digital cases. A specialist of this kind can be valuable when accurate device fitting, padding and compact protective structures matter more than large travel capacity. When evaluating a specialist, ask how much of the development is built around your dimensions and how much relies on resizing existing patterns, because those two approaches can produce very different results.
YCT Bag represents another manufacturing model: larger programs aimed at business and laptop backpacks. A higher MOQ can suit established brands, distributors or retail programs that already know their annual demand. It can also make custom materials and dedicated component purchasing more practical, although the commercial advantage disappears if the brand is forced to carry inventory faster than it can sell.
BUBM has a strong public emphasis on laptop products and electronic-accessory organization. This can be useful for companies wanting to build a coordinated product line around laptops, charging accessories, cables and mobile electronics. When sourcing several related products from one manufacturing system, consistency in material, color, branding and packaging can become as important as the individual quality of each item.
Junyuan Bags, KIVIN, Osgoodway and Panway fit more broadly into the backpack-manufacturing category. Their relevance increases when the computer compartment is one part of a larger travel, sports or daily-carry product. A backpack manufacturer should be evaluated not only on laptop padding but also on shoulder-strap shape, body balance, compartment organization, back-panel construction and the effect of realistic loading.
UMO VINA provides a Vietnam-based alternative for companies looking to diversify Asian manufacturing. Country diversification can be commercially useful, but the location of the assembly factory tells only part of the story. Ask where fabrics, zippers, hardware and webbing originate, particularly when repeatability and lead time matter. A production country change does not automatically mean the upstream supply chain has also changed.
Vancharli Outdoor is relevant when laptop functionality overlaps with travel, outdoor or more technical construction. Multi-country production networks can provide flexibility, but they make factory identification important. The approved development sample should ideally be linked to the site producing the bulk order so that patterns, materials and workmanship standards are transferred accurately.
ECO-ZY deserves attention when recycled-material positioning forms part of the product concept. Recycled polyester and other sustainability-related materials can provide a useful commercial story, but the material claim should be supported through the specific supply chain being used for the order. A recycled textile still has to satisfy abrasion, color, coating, hand-feel and structural requirements if the laptop bag is expected to remain in use for several years.
Gentle Bags, Uinta Design and Ecophay sit closer to development-led custom programs. These types of suppliers can be attractive to teams that have a clear market idea but do not yet have a finished production specification. The value lies in converting requirements such as device size, intended contents, target price, material preference and desired appearance into a sample that can eventually become a controlled production standard.
EDIOM SPORTS is more specialized around neoprene products, which makes it particularly relevant for close-fitting laptop sleeves. Neoprene allows padding and surface fabric to be combined in a relatively compact construction, but thickness, density, lamination and edge finishing still have to be controlled carefully. A sleeve should be developed around actual device dimensions rather than screen size alone.
Mherder and BagsPlaza are more relevant to leather laptop products and executive accessories. Leather and PU constructions bring different concerns from technical backpacks. Surface consistency, grain, color variation, edge paint, hardware finish, lining, magnetic closures and long-term folding performance may matter more than ultralight weight or technical waterproofing.
Tamador can be considered when laptop carrying is combined with travel or business backpack functionality. As features accumulate, however, development discipline becomes increasingly important. Adding more pockets, USB openings, hidden zippers, expansion panels and security details may make a product look more competitive on paper while also increasing weight, sewing time, cost and possible failure points.
GenXport and Ecobagfactory can be relevant for corporate, promotional or employee-equipment programs where branding, packaging, delivery schedules and controlled customization are important. These projects may not require highly technical protection systems, but they often involve strict logo positioning, color consistency, barcode or packaging requirements and fixed event deadlines.
JU MEI Bags, Guangzhou Haoen Leather, China Blooming Manufacture, Xiamen Chuanghuasheng and Qingdao Bailiwei Bags broaden the sourcing pool further. Companies evaluating these suppliers should request current examples closest to the intended construction and avoid assuming that a broad catalogue proves equal expertise across every category. The strongest comparison is always between suppliers quoting the same controlled specification.
How to Read the List
The manufacturer list becomes more useful when viewed through three different product scenarios. A fifteen-dollar promotional sleeve used in an employee welcome kit may prioritize cost, branding clarity and delivery. A ninety-dollar commuter backpack carrying a laptop five days per week needs stronger attention to ergonomics, abrasion resistance and electronics protection. A one-hundred-and-eighty-dollar leather work bag depends heavily on leather grading, edge finishing and premium hardware.
Those examples explain why choosing one universal “best” manufacturer is not particularly meaningful. Laptop specialists are useful when device protection and accurate fit dominate the design. Backpack specialists become more relevant when load distribution, comfort and organization are central. Material specialists matter when leather, neoprene, recycled textiles or technical coatings define the product’s value. Development-oriented OEM/ODM factories are especially useful when the starting point is still a product idea rather than a finished tech pack.
Volume also changes the decision. A factory built around large production runs may offer more efficient material purchasing and stable dedicated lines once specifications are mature. A supplier comfortable with a few hundred units may provide greater flexibility during market testing. Neither production model is automatically superior because they solve different commercial problems.
Before contacting twenty-five manufacturers, it is usually more efficient to identify perhaps five to eight serious candidates whose manufacturing model matches the product. The quality of the RFQ and qualification process will usually have a greater effect on the outcome than the number of factories contacted.
What to Verify Before Contact
Start with evidence of comparable products. The reference product does not need to look identical, but its construction should share meaningful similarities with your project. For a technical backpack, inspect compartment structure, padding, strap attachment, body stability and hardware. For a slim sleeve, focus more heavily on device fit, foam, edge construction, closure and surface finish.
Then confirm commercial conditions for the actual specification. A public MOQ is useful for early screening, but custom-dyed fabric, special buckles, molded parts or complex packaging can change the effective minimum. Ask whether MOQ applies per style, per color or across a combined order. Multi-color development can become surprisingly expensive when each color triggers separate upstream material minimums.
Development capability should also be tested directly. If a supplier claims ODM capability, ask what it can do when presented with only a reference image, device dimensions, target retail price and intended use. A genuine development team should discuss materials, construction, cost and production feasibility rather than simply offering a similar catalogue item.
Finally, ask how an approved sample becomes bulk production. Manufacturers with mature systems should be able to discuss pattern versions, material confirmation, BOM control, approved color references, golden samples, first-piece checks, in-line inspection and final inspection. Those answers reveal far more than a generic promise that every bag is checked carefully.
Which Laptop Bag Types and Materials Should Brands Compare?

Laptop bag selection should begin with the intended use rather than with a fabric catalogue. Sleeves prioritize accurate fit and compact cushioning, business cases require structured presentation and reliable handles, while backpacks must manage protection, weight distribution and carrying comfort. Materials such as polyester, nylon, Oxford, canvas, neoprene, PU and recycled fabrics should then be compared according to weight, abrasion resistance, structure, appearance, coating and cost.
Laptop Bag Types
Laptop sleeves provide the most compact protection and are often designed to sit inside a larger backpack, tote or suitcase. Their relatively simple appearance can hide strict dimensional requirements because there is little spare space to compensate for an incorrectly sized pattern. Device clearance, foam compression, zipper position, edge finishing and whether the computer is used with an additional protective shell should all be settled during development.
Business briefcases carry more than the computer itself. Chargers, documents, notebooks and accessories increase weight, which places more demand on the handles and shoulder-strap attachment points. Structured side panels may also be necessary if the bag is expected to maintain a professional silhouette when it is partly empty. The manufacturer should consider where weight concentrates instead of treating the briefcase like a lightweight fashion handbag.
Messenger bags provide faster access and hands-free carrying but place much of the load on one shoulder. Strap width, hardware orientation and anchor reinforcement therefore matter. A narrow webbing strap may look clean on a product photograph but become uncomfortable during a forty-minute commute when the bag carries several kilograms of electronics and personal items.
Laptop totes combine workplace function with a more lifestyle-oriented shape. One common mistake is designing the handles in the same way as a normal fashion tote. A laptop concentrates significant weight in a small area, so handle attachment zones, body material and base structure may require additional reinforcement. The product can still look clean and refined without hiding the fact that it is performing a load-bearing function.
Backpacks distribute the load across two shoulders and are generally the most practical format for commuting and travel. Once a pack reaches roughly twenty to thirty litres, the design should consider shoulder-strap curvature, back-panel padding, compartment placement and overall centre of gravity. A well-organized empty bag can still become uncomfortable if heavier objects are positioned too far from the wearer’s back.
Travel laptop backpacks add even more complexity because electronics must coexist with clothing, chargers, toiletries and sometimes shoes. The laptop compartment should remain isolated from hard accessories and the body needs enough structure to prevent packed items from forcing pressure into the computer area. Every additional pocket and expansion feature should have a real purpose because complexity adds pattern pieces, sewing operations, weight and production risk.
Material Performance
The name of a material does not describe its complete performance. Polyester, for example, can range from lightweight promotional textiles to heavy coated constructions suitable for travel products. Nylon shows a similar range. Specifications such as denier, yarn structure, weave, backing, coating, finished weight and surface treatment are often more useful than the fiber name alone.
Polyester in the approximate 300D to 600D range is commonly seen in mainstream backpacks and corporate programs because it balances cost, durability and printing compatibility. Heavier constructions such as 900D or 1680D may be used where a more substantial hand feel or greater abrasion resistance is desired, although higher denier does not automatically mean better finished-product performance.
Nylon is often chosen for premium commuter and travel bags because it can provide an attractive combination of strength, relatively low weight and technical appearance. High-density and ballistic-style constructions can perform well in demanding applications, but they may be unnecessary for a simple laptop sleeve where a lighter, less expensive fabric meets the intended use.
Oxford fabric is another term that should be treated carefully. Oxford describes a weave structure rather than one universal material specification. A sourcing team should still confirm whether the fabric is polyester or nylon, what denier is being used and whether PU, PVC or another backing or coating has been applied.
Canvas provides a natural, substantial appearance that works particularly well for lifestyle laptop totes, casual work bags and heritage-inspired products. It can be heavier than synthetic alternatives and may absorb more moisture unless treated, but some brands deliberately choose those characteristics because the hand feel and visual ageing fit their identity.
Neoprene is widely used for compact sleeves because its foam body provides cushioning without requiring a complicated layered structure. Thickness and density still matter, as does the textile laminated to the foam. A thin, soft neoprene and a firmer multi-millimetre construction can produce very different fit and protection even if both products are simply described as “neoprene sleeves.”
PU leather creates a cleaner business or fashion appearance at a lower material cost than genuine leather, but quality varies considerably. Surface stability, hydrolysis resistance, backing, thickness and repeated folding areas should be considered when the product is expected to remain attractive for several years.
| Material | Common Strength | Typical Laptop Product | Main Point to Check |
| Polyester | Cost-efficient and versatile | Mainstream backpacks | Denier, backing and coating |
| Nylon | Lightweight and abrasion resistant | Premium commuter bags | Density, coating and cost |
| Oxford | Structured woven appearance | School and business bags | Fiber type and denier |
| Canvas | Natural and substantial feel | Lifestyle totes | Weight and moisture behavior |
| Neoprene | Flexible cushioning | Laptop sleeves | Thickness and density |
| PU leather | Refined business appearance | Briefcases and sleeves | Surface durability |
| RPET | Recycled-content positioning | Retail and corporate bags | Material verification |
| TPU-coated fabric | Strong weather resistance | Technical commuter bags | Seam and zipper construction |
Protection and Structure
Laptop protection begins with correct internal dimensions. A compartment must provide enough clearance for insertion without allowing excessive movement. If the computer is normally used with a hard shell, that additional thickness needs to be included in development. A sample that fits a bare laptop perfectly may become unusable once a common protective case is added.
A suspended laptop compartment can be particularly useful in backpacks. By positioning the bottom of the computer pocket above the exterior base, the design reduces direct impact when the bag is placed on the floor. The actual benefit depends on the clearance remaining after the bag is loaded, so the sample should be checked with realistic contents rather than only while empty.
Corner coverage deserves similar attention. Adding thick foam to the front and back panels while leaving the lower corners relatively exposed creates an incomplete system. Protective materials should be arranged around the likely impact path, and hard objects such as chargers should be separated from the computer where possible.
Water protection should also be described accurately. Coated nylon or polyester may resist water penetration through the textile, but ordinary stitched seams, zipper openings and needle holes can remain vulnerable. A conventional sewn backpack may therefore be appropriately described as water-resistant while a genuinely waterproof construction requires a more integrated approach involving material, seam treatment, zipper selection and testing.
The material and structure need to work together. Lovrix’s documented pattern-development framework similarly treats laptop protection, internal compartments, load-bearing points and structural reinforcement as part of the same engineering process rather than isolated features.
How Do OEM, ODM, MOQ and Sampling Work?

OEM is usually the better route when the laptop bag has already been technically defined, while ODM becomes valuable when the manufacturer needs to help translate a concept into a production-ready structure. MOQ is influenced by finished quantity, fabric, colors, hardware, branding and packaging. Sampling then confirms dimensions, fit, materials, construction and appearance before those decisions are converted into controlled bulk-production specifications.
OEM and ODM
An OEM program usually begins with relatively complete information. The brand may provide a tech pack containing finished dimensions, pocket measurements, main fabric, lining, foam, webbing, zipper specifications, artwork, packaging requirements and acceptable tolerances. A physical reference sample can perform a similar role when the product team clearly identifies what should remain unchanged and what needs improvement.
The manufacturer’s main responsibility in an OEM project is accurate execution combined with manufacturability review. Even a complete design may contain features that are expensive, difficult to sew consistently or poorly matched to the intended material. A capable factory should identify those issues before production rather than following the drawing blindly and allowing problems to appear later.
ODM begins earlier in the development process. A company may know that it needs a lightweight sixteen-inch commuter backpack aimed at professionals and sold around a particular retail price but may not yet know the correct fabric, foam, pocket architecture, back-panel construction or zipper system. In that situation, the manufacturer becomes part of the product-development team.
The distinction matters because not every factory that advertises ODM provides the same level of design support. Some suppliers may only modify existing catalogue items, while stronger development teams can work from user scenarios, target price, product references and material expectations to build a new structure.
Lovrix supports both models. Its documented OEM workflow covers products based on drawings, physical samples, tech packs and confirmed specifications, while ODM development can begin with ideas or reference images and continue through materials, structural planning and sampling.
The correct choice depends on how much product definition already exists. A highly capable execution factory can be an excellent OEM partner even if it contributes relatively little original design, while a genuine ODM program requires pattern makers, material knowledge and enough technical communication to explain compromises between protection, appearance, cost and manufacturability.
MOQ and Cost Structure
MOQ is often misunderstood because sourcing teams focus only on the finished-bag number. In reality, a custom laptop bag combines several supply chains with their own production economics. The sewing factory might agree to assemble five hundred units while a fabric mill, zipper supplier or packaging printer requires a different quantity before it will create a dedicated color or component.
Imagine an order of one thousand laptop backpacks divided into five custom colors. Two hundred bags per color may be acceptable to the sewing line, but a textile mill might not be willing to dye such small quantities individually. The practical solution could be reducing the number of colors, selecting stock shades or consolidating more products around the same material.
Custom jacquard webbing, molded buckles, unique metal zipper pullers, branded hardware and printed gift boxes can introduce similar constraints. The effective MOQ therefore comes from the most restrictive part of the supply chain, not simply from sewing capacity.
Lovrix uses a documented standard MOQ of 500 pieces per design, while material, product structure, logo process, packaging and project complexity can influence the final requirement. Other manufacturers in the category may begin below that level, while factories oriented toward larger production programs may work more efficiently from approximately one thousand pieces or higher.
None of those numbers makes one manufacturing model automatically better. A two-hundred-piece run may be ideal for testing a new product. A one-thousand-piece minimum may be perfectly reasonable for an established retailer with predictable demand. Problems arise when MOQ is evaluated independently from inventory turnover, color planning and sales forecasts.
Cost should be broken down in the same practical way. Exterior fabric, lining, foam, webbing, zippers, hardware, pattern complexity, number of compartments, branding, packaging, inspection and quantity all contribute to the final price. Simplifying one hidden pocket or eliminating an unnecessary zipper can sometimes produce a more meaningful saving than replacing the visible main material with something obviously cheaper.
Sampling and Approval
Sampling converts an idea into something that can be measured, carried and challenged. For relatively conventional custom bags, first samples may often require roughly five to fifteen working days, although the actual schedule depends on materials, structure and component availability. Custom-dyed textiles, jacquard webbing, molded parts or unusual hardware can extend the process because development cannot begin fully until those inputs are available.
The first sample should be treated as a development prototype rather than automatically accepted as the final production reference. Load it with the actual or representative computer and accessories, wear it, operate every zipper, check every pocket and compare the finished dimensions with the intended specification. Product photographs alone rarely reveal pressure points, poor access or uncomfortable weight distribution.
Every revision should be recorded numerically whenever possible. Instructions such as “make the strap wider” or “add more padding” leave room for interpretation. A better revision states the current measurement, requested measurement and affected area. That creates a history that can be transferred accurately into the next sample and eventually into production.
Once the final version is approved, it should become the golden sample or equivalent production standard. Pattern versions, BOM, material references, artwork and packaging should all match that version. Production should not continue changing design details informally after approval because uncontrolled development on the sewing line is one of the easiest ways for sample-to-bulk inconsistency to appear.
How Do Manufacturers Test Laptop Protection and Quality?
Laptop bag quality should be checked through product-specific controls rather than one broad inspection at the end. Manufacturers should verify materials, device fit, padding, stitching, zippers, strap anchors, handles, hardware and packaging at appropriate stages. Performance claims such as waterproof, impact-resistant or load-bearing should be linked to defined test conditions because the final construction, rather than one individual component, determines how the bag performs.
Laptop Protection Checks
The first protection test is simply whether the intended laptop fits correctly. Use the real device or an accurate dimensional model and check insertion, removal, corner clearance and zipper position. The laptop should not scrape against zipper teeth, exposed hardware, rivets or rough internal seams. A compartment that is too tight creates pressure, while one that is too loose allows the device to move inside the bag.
The next step is checking the structure under realistic loading. A laptop compartment may appear well protected in an empty backpack but behave differently after the front organizer contains a charger, power bank and other hard accessories. The loaded bag should be examined to see whether those items press against the computer or distort the compartment.
Bottom protection is especially important. If the laptop pocket is suspended, measure the distance between the bottom of the device and the exterior base of the bag. Then load the remaining compartments and check whether that clearance remains. A suspended compartment offers little benefit if the structure collapses under normal packing.
Impact claims should be handled carefully. A generic padded bag does not automatically become “drop-proof.” If a brand intends to publish a measurable protection claim, the test protocol should define the test weight or device, drop height, orientations, number of cycles, impact surface and pass-or-fail criteria. Without those conditions, one impressive number can be misleading.
The same caution applies to water performance. Spray resistance, rain exposure, hydrostatic-pressure testing and submersion are completely different conditions. Product descriptions should reflect what has actually been tested rather than adopting the strongest marketing language available.
Straps, Zippers and Seams
Many laptop-bag failures occur outside the laptop compartment. A computer, charger, bottle, documents and power bank can create a substantial daily load, and that load is repeatedly transferred through the shoulder straps, handles and body seams. A bag may survive a short showroom demonstration while developing problems only after weeks of commuting.
Load capacity should therefore be evaluated as a complete structural path. Webbing strength alone does not prove that the finished bag can carry the same force. Thread, seam allowance, bartacks, box stitching, reinforcement patches, body material, hardware and the direction of force all influence the final result.
Handle and strap evaluations can include seam-pull checks, bartack inspection, repeated loaded carrying and hardware-pull testing where appropriate. The exact method should match the intended risk and product position instead of using one arbitrary load number for every design.
Zippers are another high-use component. During development, check the zipper while the bag is realistically loaded rather than only while empty. Curves, corners and heavily packed sections can create tension that makes a zipper feel significantly different from the first sample viewed on a table.
Stitch density should also be matched to the material. More stitches per inch do not automatically produce a stronger seam because excessive needle penetration can weaken certain coated or tightly woven fabrics. Thread, needle, seam construction and direction of force need to work as one system.
Bulk Quality Control
Quality control should start when materials arrive rather than when finished bags are packed. Main fabric can be checked for color, surface condition, coating and obvious defects, while foam, webbing, zippers, buckles, lining and hardware can be compared against approved references before cutting begins.
Cutting accuracy is particularly important for laptop products because relatively small differences can change the internal fit or zipper alignment. The first completed units from the production line should therefore be checked against the approved sample before the factory produces the full order at speed.
| Production Stage | Laptop Bag Check | Main Risk Controlled |
| Incoming material | Fabric, foam, zipper and webbing | Wrong or inconsistent components |
| Cutting | Pattern dimensions and orientation | Size and shape variation |
| First-piece approval | Laptop compartment and straps | Misinterpreted production standard |
| In-line sewing | Stitching, bartacks and zippers | Repeated workmanship defects |
| Assembly | Hardware and structural alignment | Functional failure |
| Final inspection | Dimensions, fit and appearance | Finished-product defects |
| Packing | Labels, shape and carton quantity | Shipping and retail errors |
For larger production runs, an AQL-based inspection plan or customer-specific sampling standard may also be used. The important point is that acceptance criteria should be agreed before production rather than introduced after the order has already been completed.
Factory certifications can support supplier qualification, but they answer different questions. A quality-management certification, social-compliance audit or recycled-material certificate may provide useful evidence about systems and supply chains, yet none of them independently proves that a particular sixteen-inch laptop fits correctly or that a shoulder strap is reinforced appropriately. Product quality still requires product-level evidence.
How Do You Choose the Right Laptop Bag Manufacturer?
Choose a laptop bag manufacturer by matching its development process, category experience, material access, MOQ, production scale and quality system to the specific product you intend to sell. Compare manufacturers using the same controlled RFQ rather than allowing each factory to quote a different interpretation. A slightly higher unit price can be worthwhile when it reduces sample revisions, production inconsistency, returns and replacement risk.
Match Factory to Product
Supplier selection should begin with the end user. A promotional laptop sleeve for an employee welcome kit has very different priorities from a premium commuter backpack or executive leather briefcase. Once the usage scenario is clear, it becomes easier to decide what kind of manufacturing expertise is actually required.
A useful product brief should identify who carries the bag, how often it will be used, the exact computer dimensions, what else must fit inside, the intended retail or wholesale price range, realistic first-order quantity and the two or three features that make the product commercially different. Those answers provide more sourcing value than beginning with a long factory list.
A neoprene specialist makes sense when the product is a compact fitted sleeve. A backpack-focused manufacturer is more suitable when ergonomics, organization and daily load are central. A leather specialist can be a better choice for executive products where material grading and finishing are critical. A development-oriented OEM/ODM partner becomes valuable when material, protection and structure still need to be worked out.
Do not automatically assume the manufacturer with the largest product catalogue has the deepest knowledge. Specialization can reduce development risk because the factory has already encountered many of the category’s common problems. At the same time, a broader manufacturing system may be more useful when the project will eventually expand from one laptop bag into a coordinated collection of backpacks, sleeves, organizers and travel products.
Compare Quotes Correctly
Quotation comparison only works when each supplier is pricing the same specification. Imagine one factory quoting a backpack at $12.80 and another quoting $14.10. The $1.30 difference appears significant until you discover that the second quotation includes stronger webbing, denser lining, better zippers, reinforced strap anchors and a more complete laptop compartment.
Those are not two prices for the same product. They are prices for two different products that happen to share a similar outline.
Before comparing unit cost, normalize the exterior material, coating, lining, foam, zipper, webbing, hardware, laptop-compartment dimensions, logo process, packaging, inspection requirements, trade terms and quantity. The difference between quotations can then be traced to real specifications instead of guesswork.
Total sourcing cost should also include failure risk. Saving one dollar on five thousand units appears to save five thousand dollars. If weaker zippers, poor laptop fit or strap failures later generate returns, replacement shipments, damaged-device claims or negative reviews, a large portion of that saving can disappear.
This does not mean choosing the highest quotation. It means understanding what has been removed or changed to reach each price. A skilled manufacturer should be able to explain alternative materials or constructions and show how they influence cost rather than simply cutting the price until the order is won.
Build a Better RFQ
A clear RFQ improves quotation accuracy and makes supplier capability easier to compare. At minimum, provide the product type, approximate dimensions, target laptop size, quantity, colors, branding and destination market. When available, add front, back and side references, a tech pack or dimension drawing, expected accessories, preferred exterior fabric, lining, protective requirements, pocket layout, logo artwork, packaging and the desired production window.
For development-heavy projects, describing the commercial target is particularly useful. “We need a sixteen-inch premium commuter backpack for professionals in the US market, designed for daily train travel and a retail price around $120” tells an experienced product team considerably more than “Please quote a black laptop backpack.”
Pay attention to the questions the supplier asks in return. A basic response might simply say that the factory can make the bag and request a quantity. A more technically engaged team may ask whether the laptop will be used with a shell, whether the compartment should be suspended, what other items the user carries, whether the fabric color needs to be custom dyed and what level of water resistance is expected.
Those questions show how the manufacturer approaches risk before production. The supplier decision should therefore consider more than the sample sitting on a desk. You are selecting the manufacturing system that must reproduce the same material, dimensions, structure, branding and protection across thousands of units and then reproduce them again when a repeat order arrives months later.
Conclusion
Finding the right laptop bag manufacturer is less about discovering a single famous factory and more about matching a manufacturing system to a specific commercial product. A slim neoprene sleeve, business briefcase, commuter backpack and technical travel bag all require different strengths, even though each one may appear under the same “laptop bag” category in search results.
The strongest sourcing decisions usually begin with accurate product requirements, realistic volume planning and a controlled comparison process. Device dimensions, materials, compartment design, padding, straps, hardware, MOQ, sampling and quality controls should all be clarified before price becomes the deciding factor.
A reliable manufacturer should be willing to discuss not only what it can produce but also where the product may fail, which materials create unnecessary cost, which features make production unstable and which design decisions need to be verified during sampling. That type of conversation is more valuable than a catalogue containing hundreds of similar-looking bags.
When product teams approach the project this way, the shortlist of twenty-five manufacturers becomes much easier to use. The objective is not to contact every factory. It is to identify several manufacturers whose materials, development capability, production model and quality system align with the exact product you intend to put into the market.
Frequently Asked Questions
What is the typical MOQ for custom laptop bags?
Custom laptop bag MOQs vary widely according to the manufacturer, structure and material. Commercial programs may begin around 200 to 500 pieces for relatively straightforward products, while larger backpack factories may prefer around 1,000 pieces or more. Custom-dyed fabrics, jacquard webbing, molded hardware, special zippers and printed packaging can raise the effective minimum even when the sewing factory itself accepts a smaller quantity. Always confirm whether MOQ applies per design, per color or across the total project.
How long does it take to manufacture custom laptop bags?
A regular first sample may require approximately five to fifteen working days when standard materials and components are available. Bulk manufacturing frequently takes several additional weeks after sample, material and artwork approval, while complex laptop backpacks with custom fabrics, specialized hardware, multiple revisions or retail packaging can require longer. The most reliable schedule separates material sourcing, sampling, revision, golden-sample approval, mass production, inspection and shipment instead of presenting one optimistic number for the entire project.
Which material is best for a laptop bag?
There is no single best material because the correct choice depends on the product’s price, appearance, weight and intended use. Polyester is widely used for mainstream and corporate bags, while nylon is common in premium commuter and travel products because of its strength-to-weight characteristics. Canvas suits lifestyle designs, neoprene works particularly well for compact sleeves, and PU or genuine leather can create a more professional appearance. Denier, weave, coating and backing often matter more than the fiber name alone.
How much padding should a laptop bag have?
Laptop protection should not be judged only by foam thickness. The right amount depends on foam density, device dimensions, the location of the padding, the outer structure and the intended protection level. A good design normally considers front and back coverage, lower corners, bottom clearance and separation from chargers or other hard objects. A suspended compartment may improve bottom protection without making the entire bag excessively thick. Any specific impact claim should be supported by an appropriate test rather than padding thickness alone.
What is the difference between OEM and ODM laptop bag manufacturing?
OEM manufacturing normally begins with an existing design, sample, tech pack or detailed specification that the factory evaluates and reproduces for production. ODM begins earlier and involves greater manufacturer participation in material selection, pattern development, compartment design, functional planning and sample creation. OEM is therefore suitable when most technical decisions have already been made, while ODM is useful when a company has a market concept, reference image or usage requirement but still needs help turning it into a production-ready laptop bag.
How can I verify a laptop bag manufacturer before placing an order?
Verification should combine company information with product-level evidence. Ask for relevant production examples, material specifications, current samples, factory or production information, quality procedures and the proposed process for your order. A development sample should be tested with the intended laptop and accessories. For larger programs, third-party factory audits or pre-shipment inspections may also be appropriate. Certifications can support due diligence, but they should not replace direct verification of product fit, construction, materials and production controls.
What information should I send when requesting a laptop bag quotation?A useful RFQ should include the product type, approximate external size, exact laptop dimensions, intended capacity, quantity by color, target material, logo artwork, pocket requirements and packaging expectations. Reference images, drawings, a physical sample or a tech pack make the quotation considerably more accurate. For an ODM project, also explain the target user, market, expected retail position and important functions. The clearer the brief, the easier it becomes to compare several manufacturers on the same product rather than receiving quotations for different interpretations.


