 Skip to content

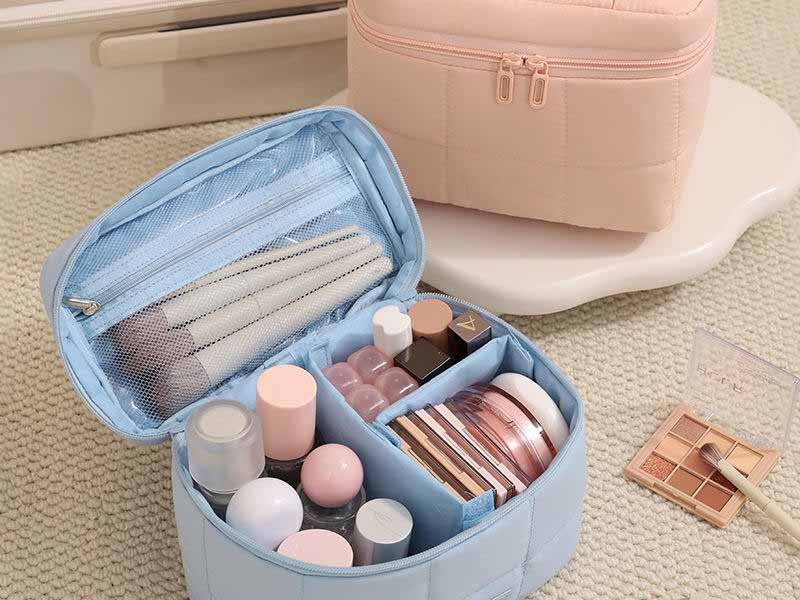
A handbag can look excellent on a sample-room table and still become an expensive problem after several thousand pieces enter production. A cosmetic bag can match the approved color, logo, and overall dimensions yet frustrate users because its lining catches in the zipper after it is filled. These situations explain why experienced product teams do not define quality simply as “looks good.” They turn every important product requirement into something that can be compared, measured, operated, inspected, or documented before the shipment leaves the factory.
A reliable handbag and cosmetic bag inspection compares bulk goods with approved specifications and physical references, then checks materials, dimensions, workmanship, zippers, hardware, linings, branding, function, cleanliness, packaging, and shipment identification. The strongest quality systems do this before production, during production, before packing, and before shipment rather than depending on one final visual check when most manufacturing costs have already been committed.
That difference matters because quality problems become more expensive as production moves forward. A logo positioned several millimeters too low can be corrected quickly after the first printed panel is inspected. The same mistake becomes much harder to solve after thousands of pieces are sewn, cleaned, packed, labeled, and loaded into cartons. The purpose of a good inspection checklist is therefore not to create more paperwork. It is to move important quality decisions to the point where they can still prevent waste, rework, shipment delays, retail complaints, and inconsistent repeat orders.
What Should a Bag Inspection Checklist Cover?
A practical bag inspection checklist should define the approved references, materials, dimensions, workmanship, components, branding, product function, packaging, defect categories, and acceptance rules. It should help the inspection team determine whether bulk production matches what was approved, not simply whether the finished bags appear attractive. The checklist should also reflect the specific handbag or cosmetic bag being produced rather than using one generic standard for every style.
Approved Quality References
The first question during inspection should not be whether a bag looks good. It should be what the bag is being compared against. Quality becomes subjective very quickly when the design team, factory, sourcing team, and inspector are working from different versions of the product specification. One team may be comparing against a development sample while another is using a revised artwork file, and both may believe they are checking the correct product.
A complete inspection package normally includes an approved physical sample, bill of materials, measurement chart, material swatches, color references, artwork files, logo placement dimensions, component specifications, packaging requirements, and any agreed functional test conditions. Each document should carry a clear revision or approval status. If a zipper puller, lining color, logo size, or packaging method changes after sampling, that change should be reflected in the controlled production information before manufacturing continues.
The approved sample remains especially useful for details that are difficult to communicate through numbers alone. Shape, hand feel, piping appearance, PU grain, edge finishing, overall stiffness, lining fit, and visual balance can often be understood more accurately by comparing with a physical reference. However, the sample should support written specifications rather than replace them. If a finished handbag is expected to measure 280 mm wide, the measurement sheet should identify the exact measurement points and agreed tolerance instead of leaving the inspector to estimate what is acceptable.
| Inspection Reference | What It Controls | Practical Example |
|---|---|---|
| Approved sample | Overall construction and appearance | Handle position, bag shape, lining fit |
| BOM | Materials and components | Outer fabric, zipper, lining, hardware, webbing |
| Measurement chart | Finished dimensions and tolerances | Width, height, gusset, handle drop |
| Material swatch | Color, texture, surface reference | PU grain, fabric shade, coating finish |
| Artwork file | Branding accuracy | Logo size, position, orientation |
| Packaging specification | Packing and identification | Barcode, polybag, folding, carton quantity |
| Test requirement | Functional acceptance | Load, zipper cycling, pull direction |
Finished-product tolerances should also match the construction. A compact cosmetic pouch may need tighter dimensional control than a large unstructured travel tote because small changes represent a larger percentage of the product size. Flexible fabrics, padded constructions, curved seams, and structured PU products also behave differently during measurement. The right tolerance is therefore the one agreed for that specific design and measurement point, not a universal number introduced only after inspection has started.
Defect Classification
Not every defect deserves the same commercial response. A removable thread tail, a broken main zipper, and an exposed sharp metal edge are clearly different problems even though all three can technically be recorded as defects. A useful quality standard separates defects according to their effect on safety, function, specification compliance, appearance, packaging, and likely customer acceptance.
Many inspection programs use critical, major, and minor classifications. Critical defects are normally associated with serious safety, regulatory, or severe-use concerns under the agreed product requirements. Major defects usually affect normal function, significant specifications, commercial saleability, or the overall acceptability of the product. Minor defects are generally smaller workmanship or cosmetic variations that do not prevent normal use but still fall outside the approved standard.
The exact classification should be product-specific. A slightly uneven decorative stitch hidden inside a low-cost promotional pouch may have limited commercial impact, while the same visual deviation on the front panel of a premium handbag could be far more noticeable. A wrong barcode may have no effect on how a cosmetic bag functions, but it can create a major warehouse or retail problem because the product may enter the wrong inventory record or reach the wrong sales channel.
Experienced teams often prepare photographs, defect examples, or physical boundary samples for appearance-sensitive details. Edge paint, PU wrinkles, piping distortion, minor scratches, stitching alignment, print coverage, and shade variation are easier to judge consistently when everyone can compare against the same reference. This helps avoid the common situation in which the factory considers a defect acceptable while the customer sees it as a clear deviation from the approved standard.
Sample-to-Bulk Control
One of the most important inspection goals is controlling the difference between a carefully produced development sample and repetitive mass production. A sample maker may spend several hours preparing one unit, adjusting difficult seams and correcting details manually. A production line must repeat the same construction hundreds or thousands of times while maintaining speed, material flow, machine settings, operator consistency, and component availability.
The approved sample should therefore be converted into measurable production controls. The BOM locks material and component choices, the pattern controls construction, the measurement chart controls size, first-piece approval confirms the production setup, and in-line inspection checks whether those conditions remain stable as output increases. When these controls are missing, a factory can produce an excellent sample without having a reliable method for reproducing it consistently.
Changes also need to be recorded rather than communicated casually. If the logo changes from 35 mm to 32 mm, the zipper puller changes after sampling, or an internal pocket moves by 10 mm, the revised information should become part of the current production record. This becomes especially important in multi-SKU programs and repeat orders, where older artwork, materials, labels, or packaging information can accidentally reappear months later.
For recurring products, retaining patterns, BOM versions, color references, approved samples, packaging specifications, and correction records creates a valuable manufacturing history. The first production run may reveal that one seam needs additional reinforcement or one zipper curve requires a different sewing method. If that knowledge is documented, the next order begins from an improved standard instead of rediscovering the same problem.
Which Materials and Components Should Be Checked?

Materials and components should be verified against the approved BOM before they enter production. Inspection normally covers material identity, color, weight or thickness, surface condition, coating, lining, reinforcement, zippers, webbing, hardware, labels, and other functional components. Incoming inspection is valuable because replacing an incorrect material before cutting is usually far easier than repairing finished bags after printing, sewing, assembly, and packing are complete.
Outer Materials
The first material check is identity. Polyester Oxford, nylon, canvas, cotton, PU leather, clear PVC, TPU, and other bag materials may appear similar in photographs while behaving very differently during cutting, sewing, folding, cleaning, and long-term use. An inspection should therefore confirm that the bulk material corresponds with the approved specification before appearance or workmanship is evaluated.
For woven materials, useful inspection points can include fabric width, GSM where specified, shade, weave consistency, coating condition, lamination quality, print registration, visible holes, stains, slubs, creases, and contamination. If a project was approved using a particular fabric weight, production material should be checked using a defined measurement method rather than judged only by touch. A lighter or heavier fabric can change stiffness, appearance, sewing behavior, abrasion performance, and perceived product value.
PU leather requires a different approach. Inspectors may focus more closely on grain, backing, thickness, gloss, wrinkles, scratches, pinholes, peeling, shade consistency, and behavior when folded around edges. A PU surface can look clean when it is flat on the material roll but show whitening, cracking, or permanent creases when turned around tight corners or compressed inside packaging.
Transparent PVC and TPU cosmetic bags need even closer surface inspection because both sides of the material remain visible. Scratches, haze, fingerprints, blocking marks, creases, dust, pressure impressions, and welding marks can become obvious under retail lighting. In these products, protective film handling and packing methods can influence final appearance almost as much as sewing quality.
Color evaluation should preferably use an approved physical reference under consistent lighting. A phone image or monitor display is not a reliable production color standard because screen brightness, camera settings, white balance, and ambient lighting can all change how the color appears. This matters particularly when several materials, such as outer fabric, zipper tape, webbing, lining, and hardware, must coordinate within the same product.
Linings and Reinforcement
Lining quality is often underestimated because customers initially focus on the outside of a handbag or cosmetic bag. In practice, poor lining construction can create some of the most annoying everyday problems, including zipper catching, loose fabric, distorted pockets, open internal seams, wrinkles, and an overall impression that the product was assembled carelessly.
The inspection should verify lining material, color, weight or thickness, coating where relevant, surface cleanliness, and visible textile defects before assembly. After sewing, the lining should sit naturally inside the shell without pulling the exterior inward or leaving so much excess fabric that it bunches into the zipper path. Cosmetic bags deserve particular attention because their compact dimensions make a few millimeters of uncontrolled lining more noticeable.
Hidden reinforcement materials are equally important. Foam, nonwoven backing, PE or PP board, reinforcement tape, and concealed webbing can determine whether a bag holds its shape or whether handles and shoulder straps remain secure under repeated use. Because these materials disappear inside the finished product, inspection should confirm their specification and location before the seams are permanently closed whenever practical.
Structured handbags illustrate the importance of hidden components clearly. Two samples can use identical outer PU and hardware but feel completely different because one uses firmer backing or different foam thickness. Cosmetic cases can also develop difficult zipper curves when excessive foam or stiff reinforcement creates too much bulk near the opening. These issues are easier to correct while materials and patterns are still accessible.
Zippers, Hardware, and Webbing
Zippers should be checked both as incoming components and after they are sewn into the finished product. Before assembly, confirm zipper type, size, tape color, chain or coil specification, slider, puller, end stops, length, and visible finish. After assembly, operate the zipper through the full opening path and look for abnormal resistance, catching, separation, waviness, misaligned ends, or interference with the lining.
Hardware inspection can include D-rings, swivel hooks, buckles, rivets, eyelets, magnetic snaps, metal logos, strap adjusters, and decorative fittings. Important checks include plating consistency, scratches, corrosion marks, sharp edges, orientation, movement, attachment security, and compatibility with connecting components. A hook can appear strong but still be unsuitable if its opening geometry allows the approved D-ring to escape during movement.
Webbing should be compared with the approved width, thickness, weave, color, surface appearance, and application. When webbing forms a load-bearing handle or shoulder strap, inspectors should pay particular attention to hidden attachment length and reinforcement. The visible portion of the strap may look correct even when the internal seam has captured too little webbing to provide stable long-term performance.
| Component | Typical Inspection Points | Useful Check |
|---|---|---|
| Outer fabric | Shade, surface, GSM, coating | Compare with approved swatch and specification |
| PU leather | Grain, thickness, scratches, folding | Measure and compare with approved material |
| Lining | Material, color, fit, seam closure | Check clearance around zipper |
| Zipper | Type, slider, tape, operation | Full opening and closing path |
| Webbing | Width, thickness, weave, color | Compare against BOM |
| Hardware | Finish, attachment, movement | Fastness check where specified |
| Foam | Thickness and location | Measure before closure where practical |
| Label | Text, orientation, position | Compare with approved artwork |
| Reinforcement | Material and placement | Verify hidden construction before sewing closes |
The commercial benefit of incoming inspection is simple. Finding that a zipper tape is the wrong shade before assembly may require replacing one component lot. Finding the same problem after thousands of products are completed can require opening seams, removing zippers, resewing the bags, cleaning them again, and repeating inspection. Quality control is most economical when it prevents value from being added to the wrong material.
How Do You Inspect Handbag Workmanship?

Handbag workmanship inspection should focus on stitching, seams, reinforcement, shape, panel alignment, handles, straps, hardware attachment, and finishing. High-stress areas deserve particular attention because they carry more structural load than decorative seams. A handbag can look excellent when displayed on a table and still perform poorly if handle roots, D-ring tabs, zipper ends, or other load-transfer areas are not constructed correctly.
Stitching and Seams
Good stitching is not simply straight stitching. It must also be secure, suitable for the selected material, visually consistent, and positioned correctly within the construction. Inspection should look for skipped stitches, broken stitches, loose or excessive tension, wandering stitch lines, puckering, open seams, untrimmed thread, incomplete backtacking, raw edges, and visible needle damage.
Stitch density should follow the approved construction rather than assuming that more stitches always create stronger seams. On some coated or synthetic materials, extremely dense needle penetration can create a perforation effect that weakens the area. Thick seam stacks can create the opposite problem because an unsuitable needle, thread, machine adjustment, or feeding method may cause skipped stitches when several layers meet.
Seam allowance deserves attention even though it is usually hidden. A finished seam can look neat while capturing too little material internally, increasing the chance of the seam opening under load. Side panels, gussets, zipper panels, pocket corners, and handle reinforcement areas are common places where seam allowance and construction accuracy influence both appearance and durability.
Visible and hidden seams also deserve different aesthetic priorities. A slight stitching deviation inside a concealed pocket may have little effect on customer perception, while the same deviation along a central front seam or decorative piping can be immediately noticeable. A good inspection standard therefore distinguishes structural importance from visual importance instead of treating every sewing line exactly the same.
Stress Points
A handbag does not distribute load evenly across its entire body. Most carrying force passes through a limited number of structural points, so those areas should receive more focused inspection. Common examples include handle roots, D-ring tabs, shoulder-strap anchors, bottom corners, side-panel joints, zipper ends, and hardware mounting points.
Depending on the construction, reinforcement may include additional fabric layers, hidden webbing, nonwoven backing, bartacks, box stitching, rivets, or a combination of methods. The inspector should confirm not only that reinforcement exists but that it is positioned correctly. A bartack that looks strong from the outside can contribute little if it misses part of the concealed reinforcement underneath.
Functional testing should follow the intended product use and agreed specification. A small fashion handbag intended for light personal items does not automatically require the same load condition as a large tote or travel bag. The meaningful test is one that defines the load, duration, direction, sample quantity, and acceptance condition for the product being manufactured.
Instead of a vague instruction such as “pull the handle strongly,” a practical internal test should state what weight or force is applied, how long it remains applied, how the product is positioned, and what constitutes failure. Possible failure evidence can include seam opening, webbing slippage, hardware movement, permanent deformation, or detachment. Defined conditions make test results much easier to reproduce and compare across production runs.
Shape and Alignment
Shape is one of the most noticeable handbag quality characteristics, yet it is also difficult to define using a few words such as premium, balanced, structured, or elegant. Inspection becomes more consistent when the overall visual impression is divided into specific observable details.
The bag should be evaluated in the same condition used for approval, whether that means empty, lightly stuffed, or filled with reference contents. Compare left and right symmetry, gusset depth, front and back panel alignment, piping continuity, corner shape, bottom stability, flap alignment, and opening geometry. Structured products should sit naturally without obvious twisting or collapse unless softness is part of the approved design.
Handles should be checked for length, drop, spacing, angle, attachment position, symmetry, edge finishing, and reinforcement. Small differences can become obvious because two handles often sit directly beside one another. Adjustable shoulder straps add more variables, including total length, minimum and maximum adjustment, slider direction, hook orientation, stitching, twisting, and hardware movement.
Packaging can also change the shape of a finished handbag. Excessive carton compression can deform piping, crease PU surfaces, flatten foam, or distort side panels. Representative products should therefore be unpacked and allowed to recover according to the agreed method before final appearance is judged. If the design requires a particular stuffing method to preserve its shape, that packaging requirement should be treated as part of product quality rather than an optional cosmetic detail.
Finishing Details
Finishing often determines whether a product feels carefully manufactured or simply acceptable. Edge paint should be examined for coverage, smoothness, cracking, overflow, contamination, and layer consistency. Piping should remain even through curves. Glue residue, chalk marks, loose threads, oil, dust, adhesive contamination, and production debris should be removed before packing.
Branding deserves particular attention because small errors are easy to see. Inspect logo dimensions, color, orientation, location, adhesion, print clarity, embroidery density, metal-logo attachment, and consistency across the lot. A logo that is structurally secure but visibly off-center can still be unacceptable because it directly affects the appearance of the brand.
Finishing standards should also take sales positioning into account. A promotional handbag and a premium retail handbag may use similar construction methods while requiring very different visual tolerances. This does not mean quality inspection should become subjective. It means the expected appearance should be established through approved samples, drawings, or boundary references before production begins.
A product can pass basic strength and dimensional checks while still failing the approved aesthetic standard. Experienced QC teams therefore evaluate structural performance and appearance separately. A strong seam does not excuse poor edge paint, and beautiful finishing does not compensate for a weak handle attachment.
How Do You Inspect Cosmetic Bag Quality?

Cosmetic bag inspection should emphasize zipper movement, lining clearance, pockets, binding, compact seam construction, transparent surfaces, cleanliness, and filled-bag function. These products often concentrate many sewing operations into a small space, so only a few millimeters of excessive lining, binding bulk, or zipper misalignment can noticeably affect everyday use even when the bag looks acceptable while empty.
Zippers and Linings
The zipper is often the most frequently used mechanical component on a cosmetic bag, particularly on styles that open around several sides. Inspection should therefore involve more than opening and closing the empty product once. The entire zipper path should be checked for waviness, twisting, inconsistent seam distance, poorly finished ends, abnormal resistance, and slider interference.
The bag should then be tested with representative contents because filling changes the way pressure is distributed through the shell. Bottles, compacts, brushes, or test blocks can push the panels outward and increase tension around corners. A zipper that feels smooth on an empty product may become difficult to operate once the cosmetic bag is filled to its intended capacity.
Lining interference is a particularly common issue. Excess lining near the zipper can be pulled into the slider, especially around curves where the fabric naturally gathers. Inspectors should check clearance through the complete zipper path and confirm that the internal construction does not become trapped during normal opening and closing.
Internal seam closure should also be inspected carefully. Cosmetic bags are small enough that users can easily see and touch much of the lining, so unfinished turn openings, raw edges, open pocket seams, or excessive thread are immediately noticeable. A clean exterior does not compensate for an interior that appears poorly assembled.
Pockets and Binding
Internal pockets should be evaluated for actual usability rather than dimensions alone. A mesh pocket, elastic pocket, brush sleeve, or organizer can match the drawing precisely while still being inconvenient if the opening is too tight or the usable depth is reduced by sewing and reinforcement.
Where possible, inspectors should place representative items into the pockets. Common brush handles, cosmetic tubes, travel bottles, or test pieces can reveal problems that a ruler cannot. Equal spacing in a technical drawing does not guarantee that every compartment remains practical after elastic tension, lining thickness, seam allowance, and binding are added.
Binding requires careful examination around curves and corners because several material layers often meet in these areas. The binding should capture the raw edge completely, and inspectors should look for missed stitches, exposed material, inconsistent width, twisting, bulky joins, and hard lumps that distort the finished shape.
Cosmetic cases may also include foam dividers, removable panels, mirrors, trays, mesh compartments, or elastic loops. Each component should remain secure and function as intended after repeated handling. The more complicated the internal organization becomes, the less useful a generic “pocket inspection” line becomes. Important functions should be identified individually.
Interior cleanliness is another practical concern. Light-colored linings expose oil, glue, chalk, thread debris, dust, and machine marks quickly. Cleaning should happen before packaging so inspection does not become a process of repeatedly reopening packed products to remove simple manufacturing residue.
Clear Materials
Clear PVC and TPU cosmetic or toiletry bags require a different appearance standard because the customer can see through the product and inspect both surfaces simultaneously. Scratches, haze, fingerprints, blocking marks, creases, pressure impressions, contamination, and inconsistent transparency should be checked under suitable lighting.
Protective film can sometimes hide defects during production, so representative pieces may need to be inspected according to an agreed film-removal method. Care is required because removing protective film itself can affect how the product is packed or presented. The inspection procedure should therefore be defined before final QC rather than improvised at the inspection table.
Where clear panels are welded or heat sealed, examine seam continuity, width, bubbles, burning, distortion, and weak areas. Where they are sewn, look at needle perforation, seam alignment, and how the material reacts around folds and corners. Transparent plastics can retain pressure marks or whitening that would be less visible on textile materials.
A clear material should not automatically be described as making the finished bag waterproof. Material water resistance, welded construction, sewn seams, zipper design, and complete-product leakage are separate characteristics. If the product is sold with a water-related performance claim, the test should reflect that specific claim and define the exposure method and acceptable result.
Packaging becomes especially important for transparent products because rubbing against metal hardware or neighboring units can scratch surfaces after final inspection. Protective separation, wrapping, and folding should therefore be reviewed during the packaging trial rather than only after bulk production is packed.
Real-Use Function
A cosmetic bag should be inspected as a storage product, not merely as a collection of sewn panels. Representative contents should be loaded into the product so inspectors can observe zipper tension, pocket access, handle performance, shape retention, seam stress, and internal organization under realistic conditions.
The correct functional check depends on the style. A flat makeup pouch, structured vanity case, hanging toiletry organizer, clear travel pouch, and train case have different risk points. A single universal checklist usually spends too much time checking low-risk areas and too little time examining the feature that makes the product valuable.
If a wide-opening zipper is the main selling point, zipper geometry and lining clearance deserve close attention. If the design features multiple brush holders, those compartments should be tested with representative brush dimensions. If the product is intended to stand upright when filled, inspectors should evaluate stability rather than only checking its empty shape.
This approach connects quality inspection to product development. The strongest checklist is built around what the customer will actually do with the bag. When use conditions are understood before sampling and bulk production, important inspection points can be engineered into the product instead of being discovered only when finished goods are ready to ship.
How Are Function and AQL Tests Performed?

Functional tests should reproduce agreed product risks under controlled conditions, while AQL sampling provides a structured method for examining a representative portion of a production lot. Test loads, cycle counts, sample quantities, defect categories, inspection levels, and acceptance rules should be defined before inspection because no single functional test program or AQL combination is appropriate for every handbag and cosmetic bag.
Functional Testing
A useful functional test answers three questions: what is being tested, under what condition, and what counts as failure. Instructions such as “check the zipper” or “pull the handle strongly” are too subjective to produce consistent results between inspectors, factories, and production runs.
For zipper testing, a specification may define whether the bag is empty or loaded, how many opening and closing cycles are performed, whether the complete zipper path must be used, and what evidence constitutes failure. Failure could include jamming, chain separation, broken pullers, excessive resistance, or repeated lining entrapment, depending on the product requirement.
Handle and shoulder-strap tests should likewise define the applied load or force, holding time, direction, sample quantity, lifting method, and acceptable deformation. The correct values should come from the product specification, intended use, applicable standard, or agreed development requirement rather than a generic number copied from another bag.
Other useful checks may include seam strength, hardware fastness, logo adhesion, capacity, closure function, abrasion performance, colorfastness, coating adhesion, or water-related tests when the product claim requires them. Not every product needs every test, and applying unnecessary tests can create cost without improving the actual risk control.
| Test | Variables to Define | Possible Failure Evidence |
|---|---|---|
| Zipper operation | Cycles, empty/loaded condition | Jamming, separation, slider failure |
| Handle load | Load, duration, sample count | Stitch opening, deformation, detachment |
| Strap pull | Force or load, direction | Webbing slip, seam damage |
| Hardware fastness | Component and load method | Rivet movement, hook failure |
| Logo adhesion | Method and duration | Peeling, lifting, cracking |
| Dimension check | Measurement points and tolerance | Finished size outside specification |
| Capacity check | Reference contents | Closure difficulty, excessive distortion |
| Water-related test | Exposure method and pass criterion | Leakage beyond agreed condition |
Water-related claims deserve careful language. A fabric may have a measured hydrostatic resistance while the finished bag contains sewn seams and a conventional zipper that allow water entry. Material performance and complete-product performance are therefore different claims. Testing should match the characteristic that will actually be communicated to customers.
Defect Categories
Defect classification connects inspection findings with commercial consequences. Critical defects normally relate to serious safety, regulatory, or severe-use concerns under the agreed product criteria. Major defects commonly include failures that prevent intended use, materially differ from approved specifications, or would likely cause customer rejection. Minor defects usually involve limited appearance or workmanship deviations that do not prevent normal use.
Specific examples should be prepared for the product being inspected. A broken main zipper, detached handle, seriously incorrect dimensions, missing component, or open structural seam can be significantly more serious than a removable thread tail. A label error may appear cosmetic but become commercially important when it affects product identification or regulatory information.
Repeated defects also deserve closer attention than isolated findings. If several units show the same logo misplacement, seam error, zipper problem, or wrong component, the defect may be systemic. Repairing only the sampled products does not correct the process that created the issue.
Inspection reports should therefore identify defect type, location, frequency, and pattern rather than recording only a total number. Four unrelated minor issues may require a different response from four examples of the same major construction failure. Experienced quality managers always ask whether the inspection found random defects or evidence that the production process itself is unstable.
AQL Sampling
AQL sampling is a method for making lot-level inspection decisions using a defined sample rather than inspecting every unit. It is not a guarantee that every product in a shipment is defect-free, and it should not be described as a substitute for incoming inspection, in-line process control, or clear manufacturing specifications.
The process normally begins with the total lot size and selected inspection level. These lead to a sample-size code and corresponding sample quantity under the applicable sampling plan. The agreed AQL values and defect categories then determine acceptance and rejection numbers for the inspection.
General Inspection Level II is commonly used in routine consumer-product inspections, although another level may be selected depending on risk, product complexity, supplier history, or customer requirements. Similarly, AQL values such as 2.5 for major defects and 4.0 for minor defects are frequently seen in commercial product inspections, but they are not universal requirements.
Premium products, new styles, safety-sensitive elements, or products with a history of returns may use tighter controls. Some programs apply zero acceptance to specifically defined critical defects, while other criteria depend on the customer’s own quality system. The important point is that defect categories and sampling rules should be agreed before the final inspection starts.
Final AQL inspection should also remain separate from production monitoring. If an early in-line check finds that eight pieces out of one hundred show the same zipper problem, that observation should trigger investigation immediately. It should not be treated as though production can continue until a final statistical sampling decision is made. In-line inspection controls the process; final sampling supports shipment disposition.
Shipment Decisions
A final inspection report should lead to a clear disposition rather than simply generate photographs and defect counts. Possible outcomes include pass, hold, conditional acceptance, sorting, rework, replacement, re-inspection, or rejection depending on the defect, frequency, customer requirements, and ability to contain the affected goods.
An isolated removable thread can usually be corrected easily. Repeated zipper failures across several cartons indicate a very different level of risk because they suggest a production or component problem. Likewise, a logo that is consistently positioned 10 mm too low cannot be solved by sorting because the entire production process may have created the same deviation.
When the inspection exceeds agreed acceptance criteria, rework should be followed by verification appropriate to the scale of the problem. A large corrective action may require a new inspection instead of assuming that every repaired product is now acceptable.
Useful records should document the defect, suspected cause, affected quantity, corrective action, verification result, and final disposition. These records become increasingly valuable when products are repeated. The next production team can review past problems before manufacturing begins instead of waiting for the same defects to return.
How Do You Control Quality Before Shipment?
Quality is most effectively controlled through four connected stages: before production, during production, before packing, and before shipment. Early controls prevent wrong materials and setup errors, in-line checks stop repeated defects from multiplying, finished-product checks verify workmanship and function, and final inspection confirms product identity, packaging, carton information, and readiness for commercial shipment.
Before Production
The least expensive quality problem is the one that is identified before production adds labor and processing cost to the wrong material or setup. Before cutting begins, the production team should confirm the approved BOM, materials, patterns, measurement chart, colors, zippers, hardware, webbing, branding, labels, packaging, and test requirements.
A pre-production meeting is particularly useful for products with several materials, multiple SKUs, custom hardware, complex logos, structural reinforcement, or special packaging. Different departments normally control different parts of the product. Purchasing deals with materials and components, cutting manages patterns, printing or embroidery manages artwork, sewing controls construction, and packing manages labels and cartons. The meeting ensures that all departments are working from the same approved information.
First-piece approval should then verify that the production setup is actually reproducing the approved standard. The first printed logo should be examined before hundreds of panels are printed. The first embroidery piece should be confirmed before the full run continues. An early zipper assembly can be checked for alignment and lining clearance before that operation is repeated on thousands of units.
The financial logic is straightforward. Correcting a logo position by several millimeters on the first component can take only a short adjustment. Discovering the same mistake after several thousand finished bags have been sewn and packed may require unpacking cartons, opening seams, replacing components, cleaning, re-inspecting, and repacking.
Pre-production control therefore turns the inspection checklist into a preventive tool. Instead of waiting for defects, the team uses known risks to establish checkpoints before those risks are multiplied by production volume.
During Production
In-line inspection is designed to identify process drift while corrective action is still practical. Useful checkpoints can include cutting accuracy, print or embroidery location, zipper installation, pockets, binding, reinforcement, seam quality, hardware attachment, shape, and semi-finished assemblies.
The best in-line records show more than whether a defect exists. They identify where and when it appeared. Useful information can include quantity checked, defect type, production operation, workstation or sewing line, time, affected quantity, corrective action, and verification result.
Suppose an early production check examines one hundred pieces and finds zipper waviness on eight units. That observation should not automatically be interpreted as a final AQL result. It is a process-control signal. Continuing to manufacture another two thousand pieces without investigating zipper tension, panel dimensions, seam allowance, machine settings, operator handling, or material stretch would allow a known risk to grow.
Inspection frequency should be adjusted according to risk. New styles, first production runs, unfamiliar materials, custom logo processes, complex structures, tight dimensions, and unusual hardware generally deserve more attention than mature repeat orders with stable performance history.
The goal is not to create the highest possible number of inspections. It is to identify the operations most likely to create expensive or repeated failures and examine them before those failures spread through the lot.
Before Packing
Pre-packing inspection is one of the last efficient opportunities to examine finished products without disturbing retail packaging. Dimensions, sewing, bag shape, zippers, hardware, handles, straps, branding, internal construction, cleanliness, surface condition, and product-specific functions should be checked before the item enters its final pack.
Minor permitted corrections such as trimming threads or cleaning removable marks are easier to complete at this stage. More serious problems should be contained and investigated rather than hidden through packing.
Multi-SKU programs require particularly careful identification. A cosmetic bag program may use one construction in several colors, two artwork versions, and different barcodes for different markets. Every bag can be physically well made while the shipment remains commercially wrong because labels, hangtags, SKU codes, or packaging are mixed.
Product identity should therefore be connected to packaging identity before final pack-out. The bag color, artwork, SKU, barcode, insert, and packaging should be checked as one complete configuration rather than as independent items.
Representative functional checks may also be repeated at this stage. Zippers can be operated, adjustable straps moved through their range, pockets loaded, closures checked, and structured products inspected for final shape. This helps confirm that the complete assembled product still performs as expected after every manufacturing operation has been completed.
Packaging and Cartons
Packaging inspection is part of product quality because retailers, warehouses, fulfillment centers, and end users receive a packed product rather than the open sample seen inside the factory.
At unit level, the inspection may cover polybags, dust bags, hangtags, barcode labels, UPC or FNSKU labels where required, warning labels, instruction cards, protective film, inserts, tissue, retail sleeves, gift boxes, and folding methods. The exact requirements should match the approved sales-channel specification.
Packaging should also protect the bag. Metal hardware may need wrapping so it does not scratch PU surfaces. Clear PVC or TPU products may need protective separation to prevent rubbing. Structured handbags may need stuffing or controlled folding to maintain shape during transport.
At carton level, verify SKU, assortment, carton quantity, shipping marks, carton labels, dimensions, weight where specified, sealing, and carton condition. Mixed-SKU shipments deserve close attention because incorrect assortment can create receiving errors even when every individual product is physically correct.
Barcode and label usability should also be considered. A technically correct barcode printed too small, damaged by a fold, or placed where scanning equipment cannot reach it can still create operational problems. Packaging should therefore be evaluated in terms of what happens after the carton leaves the factory.
Failed Inspection
A failed inspection should trigger containment before anything else. The team should identify which SKU, cartons, production period, component lot, workstation, or operation may be affected so questionable goods do not continue toward shipment while the cause is still being investigated.
The next step is determining whether the problem is isolated or systemic. One stain may require cleaning and local sorting. A wrong zipper specification used across an entire production run requires much wider containment. A repeated logo-position error suggests that the printing setup itself needs correction.
Possible actions include sorting, rework, replacement, relabeling, repacking, component replacement, shipment hold, or re-inspection. The appropriate response depends on defect severity, scale, timing, customer requirements, and whether corrected products can be verified reliably.
Root-cause analysis is important because correction without prevention simply moves the same problem into the next production run. If a handle seam opens, the team should examine seam allowance, thread, stitch construction, reinforcement position, material properties, machine settings, and operator method instead of only resewing the affected units.
Long-term product programs benefit from retaining these corrective-action records together with the BOM, pattern, materials, approved samples, and packaging history. When another colorway, seasonal version, or repeat order begins, the production team already knows which details created risk previously.
Conclusion
A useful handbag and cosmetic bag inspection checklist is not simply a final sheet that records scratches, loose threads, or dimensional differences. It is a practical link between product development, approved specifications, manufacturing controls, finished-product performance, packaging, and shipment decisions. The earlier these requirements are defined, the easier it becomes to prevent the familiar problems of excellent samples followed by inconsistent bulk production.
The strongest quality systems begin with clear materials, BOMs, patterns, measurements, approved samples, and test requirements. They continue through first-piece approval and in-line inspection, then verify complete products before packing and use a defined final inspection plan before shipment. They also keep useful records so repeat orders benefit from what was learned during earlier production instead of starting from zero each time.
For handbag and cosmetic bag programs, small details can create surprisingly large commercial consequences. A few millimeters of excess lining can interfere with a zipper. A hidden reinforcement layer can determine whether a handle remains secure. A wrong barcode can turn correctly manufactured goods into a warehouse problem. A clear PVC panel can leave the sewing line in good condition and still become scratched through poor packaging.
This is why quality control works best when it is considered during product development rather than added at the end. Manufacturers that understand materials, construction, sampling, production, inspection, packaging, and repeat-order control can help product teams identify these risks earlier. When a new handbag or cosmetic bag is being developed, discussing its inspection criteria before bulk production usually creates a clearer standard, fewer surprises, and a much more stable path from approved sample to commercial shipment.
Frequently Asked Questions
What should be checked during a handbag quality inspection?
A handbag inspection should cover approved materials, measurements, stitching, seams, reinforcement, handles, straps, zippers, hardware, lining, branding, shape, cleanliness, function, packaging, and SKU identification. The inspector should compare these points against current approved samples and specifications rather than judging the product only by appearance. High-stress areas such as handle roots, D-ring tabs, bottom corners, and zipper ends generally deserve particular attention because failures there can affect normal product use.
What are the most common cosmetic bag defects?
Common cosmetic bag problems include zipper catching, excess lining entering the slider, uneven binding, missed stitches, open internal seams, pocket-size problems, surface marks, incorrect logo placement, poor cleanliness, and scratched transparent panels. Curved zipper styles can be particularly sensitive because material thickness, foam, seam allowance, and lining position all influence zipper movement. The best inspection also tests the bag with representative contents because some functional problems only appear when the product is filled.
What AQL is commonly used for bag inspection?
Commercial consumer-product inspections often reference AQL values such as 2.5 for major defects and 4.0 for minor defects, with stricter treatment for critical defects, but these figures should not be treated as universal requirements. The correct sampling plan depends on product risk, inspection level, customer standards, lot size, supplier history, and sales-channel requirements. AQL should be agreed before inspection, and passing an AQL sample does not mean every unit in the shipment has been individually inspected.
How do you inspect handbag stitching quality?
Handbag stitching inspection should check skipped or broken stitches, thread tension, stitch-line alignment, puckering, seam allowance, backtacking, raw edges, needle damage, open seams, and thread finishing. Inspectors should pay closer attention to structural areas such as handles, straps, side seams, zipper panels, and reinforcement points. Decorative seams need visual consistency, while hidden seams need sufficient material capture and strength. Good stitching inspection therefore evaluates both appearance and construction rather than simply asking whether a stitch line looks straight.
Should bags be inspected only before shipment?
No. Relying only on final inspection means many defects are discovered after most manufacturing cost has already been added. A stronger system checks incoming materials and specifications before production, approves first pieces, monitors important operations during production, examines finished goods before packing, and then performs final or pre-shipment inspection. This approach allows wrong materials, logo errors, zipper problems, sewing defects, and packaging mistakes to be corrected earlier, when fewer pieces are affected and rework is more manageable.
How do you make sure bulk bags match the approved sample?
The approved sample should be supported by a controlled BOM, pattern version, measurement chart, material swatches, artwork, component specifications, packaging requirements, and production records. First-piece approval should confirm that the bulk-production setup reproduces the approved construction before full production proceeds. In-line inspection then checks whether the result remains stable as volume increases. For repeat orders, keeping approved samples, color references, BOM revisions, patterns, and previous corrective-action records helps reduce sample-to-bulk and batch-to-batch differences.
What should be checked before handbag or cosmetic bag shipment?
Before shipment, inspection should confirm finished-product appearance, dimensions, stitching, zippers, hardware, handles, straps, lining, branding, cleanliness, function, SKU identity, individual packaging, barcode information, carton quantity, carton marks, and other agreed requirements. Any failed criteria should be contained, investigated, corrected where appropriate, and verified before release. The final shipment decision should be based on the approved inspection plan and product specifications rather than a general impression that the goods appear acceptable.


